English
 中文简体
Made of PBS (Polybutylene Succinate), fully biodegradable.Features:1.Home compostable2.Raw material: PBS Polybutylene Su...
READ MORE
Content
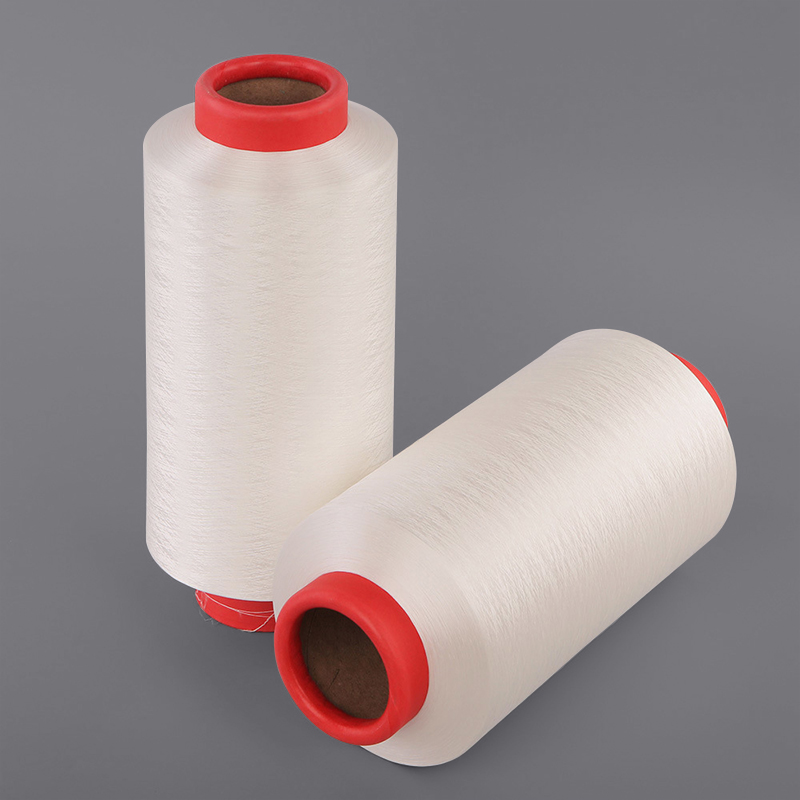
PLA Biodegradable Monofilament Yarn is a plant-based technical fiber developed for manufacturers seeking an alternative to conventional petroleum-based nylon and polyester monofilaments. Made from polylactic acid, commonly known as PLA, the yarn combines a smooth single-filament structure with renewable raw materials, controlled dimensional stability, useful tensile performance, and an end-of-life pathway based on industrial composting.
As environmental regulations become stricter and product manufacturers face growing pressure to reduce fossil-resource consumption, biodegradable yarns are becoming increasingly important. However, a sustainable material must also perform reliably during processing and use. A yarn that is environmentally attractive but difficult to weave, knit, extrude, dye, or handle may not provide a practical commercial solution. PLA monofilament addresses this challenge by combining material innovation with controlled melt extrusion and application-oriented production.
This product is suitable for technical textiles, agricultural materials, filtration media, packaging components, tea bag strings, specialty fabrics, brush applications, and other products requiring a consistent single-strand filament. It is available in a standard 30D specification, with special production available by order. Depending on the final application, additional diameter, strength, color, and processing requirements can be discussed during product development.
A monofilament yarn consists of one continuous filament rather than many smaller filaments twisted or bundled together. This structure gives the material a smooth surface, consistent diameter, low hairiness, and predictable behavior during weaving, knitting, net formation, filtration, and other conversion processes.
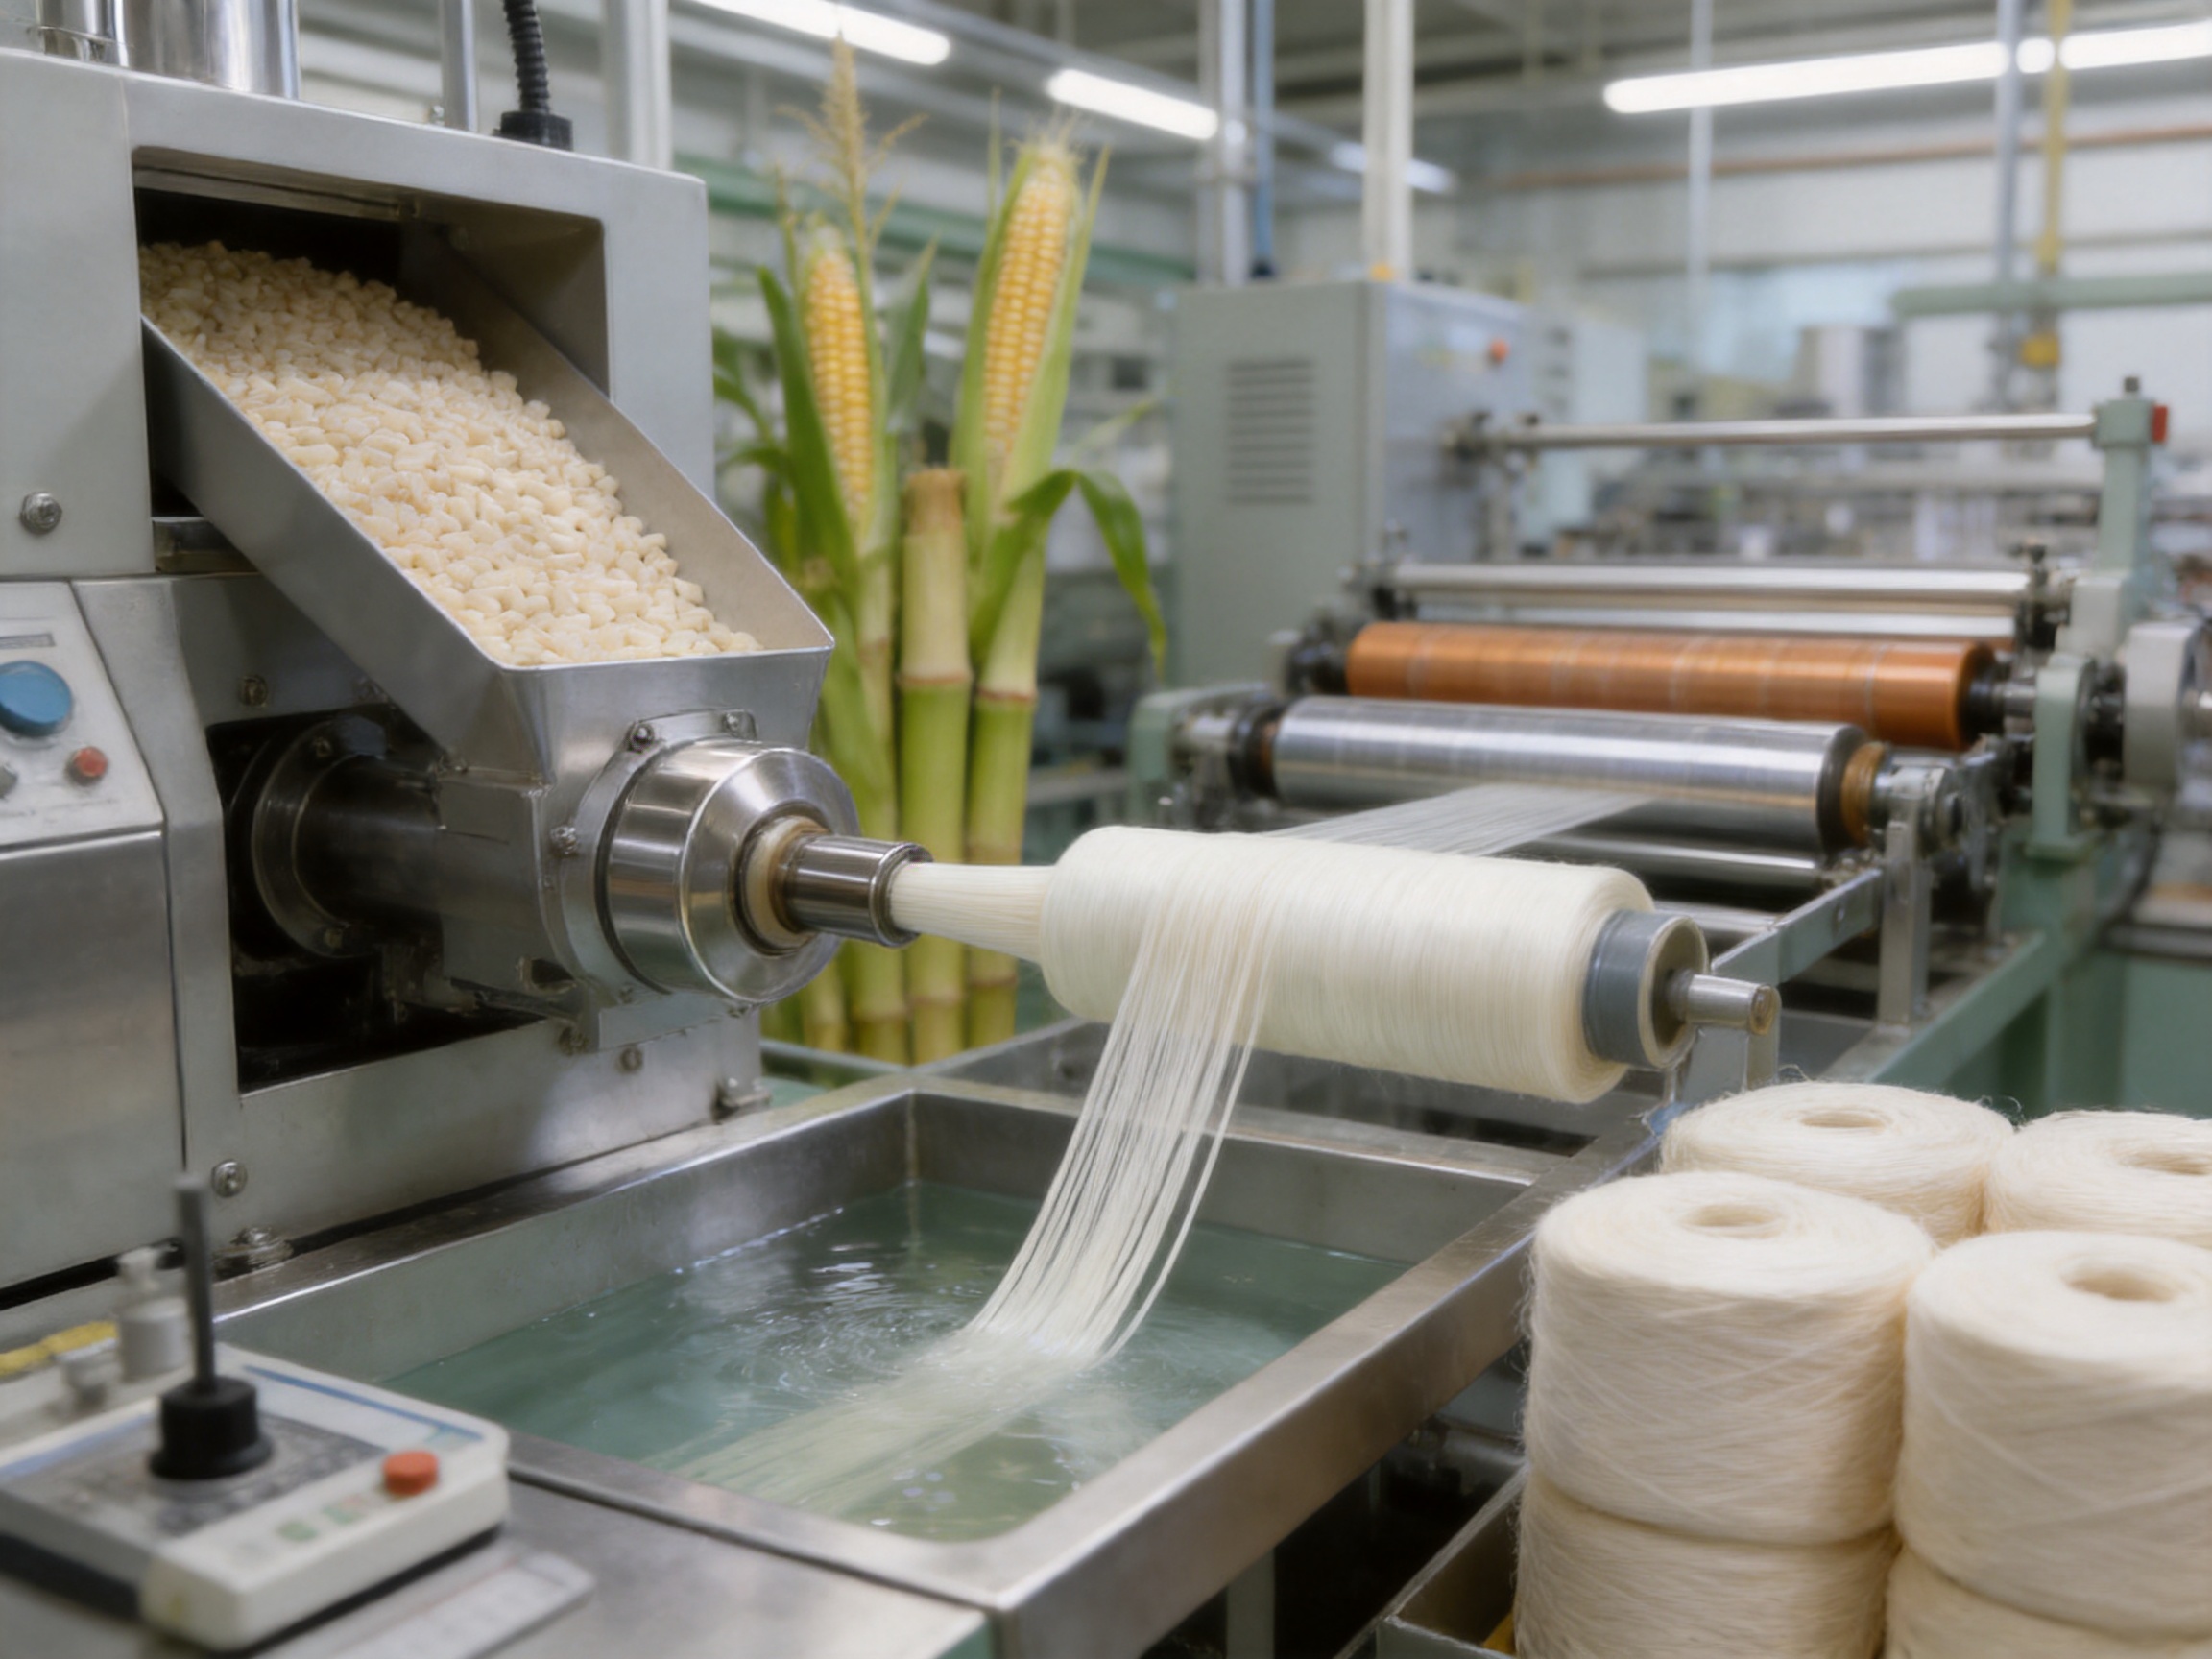
PLA is a thermoplastic polymer produced from lactic acid. The lactic acid used for industrial PLA can be derived from renewable plant-based resources such as corn starch or sugarcane. Through fermentation, purification, polymerization, and compounding, these renewable feedstocks are converted into a polymer resin suitable for fiber and filament production.
During manufacturing, PLA resin is melted and pushed through a precision spinneret. The extruded strand is cooled, drawn, stabilized, and wound into a continuous yarn package. Each stage influences final performance. Melt temperature affects polymer integrity, spinneret accuracy affects diameter uniformity, cooling affects crystallization and orientation, drawing affects tensile properties, and winding affects package quality and unwinding behavior.
The result is a technical filament that can provide a practical alternative to standard synthetic monofilaments in applications where renewable sourcing and industrial compostability are important purchasing criteria.
The primary environmental advantage of PLA monofilament is its renewable feedstock. Conventional polyester and nylon are generally produced from fossil-based raw materials, while PLA can be made from plant-derived sugars and starches. This difference allows manufacturers to reduce dependence on petroleum-based polymers and support a more circular material strategy.
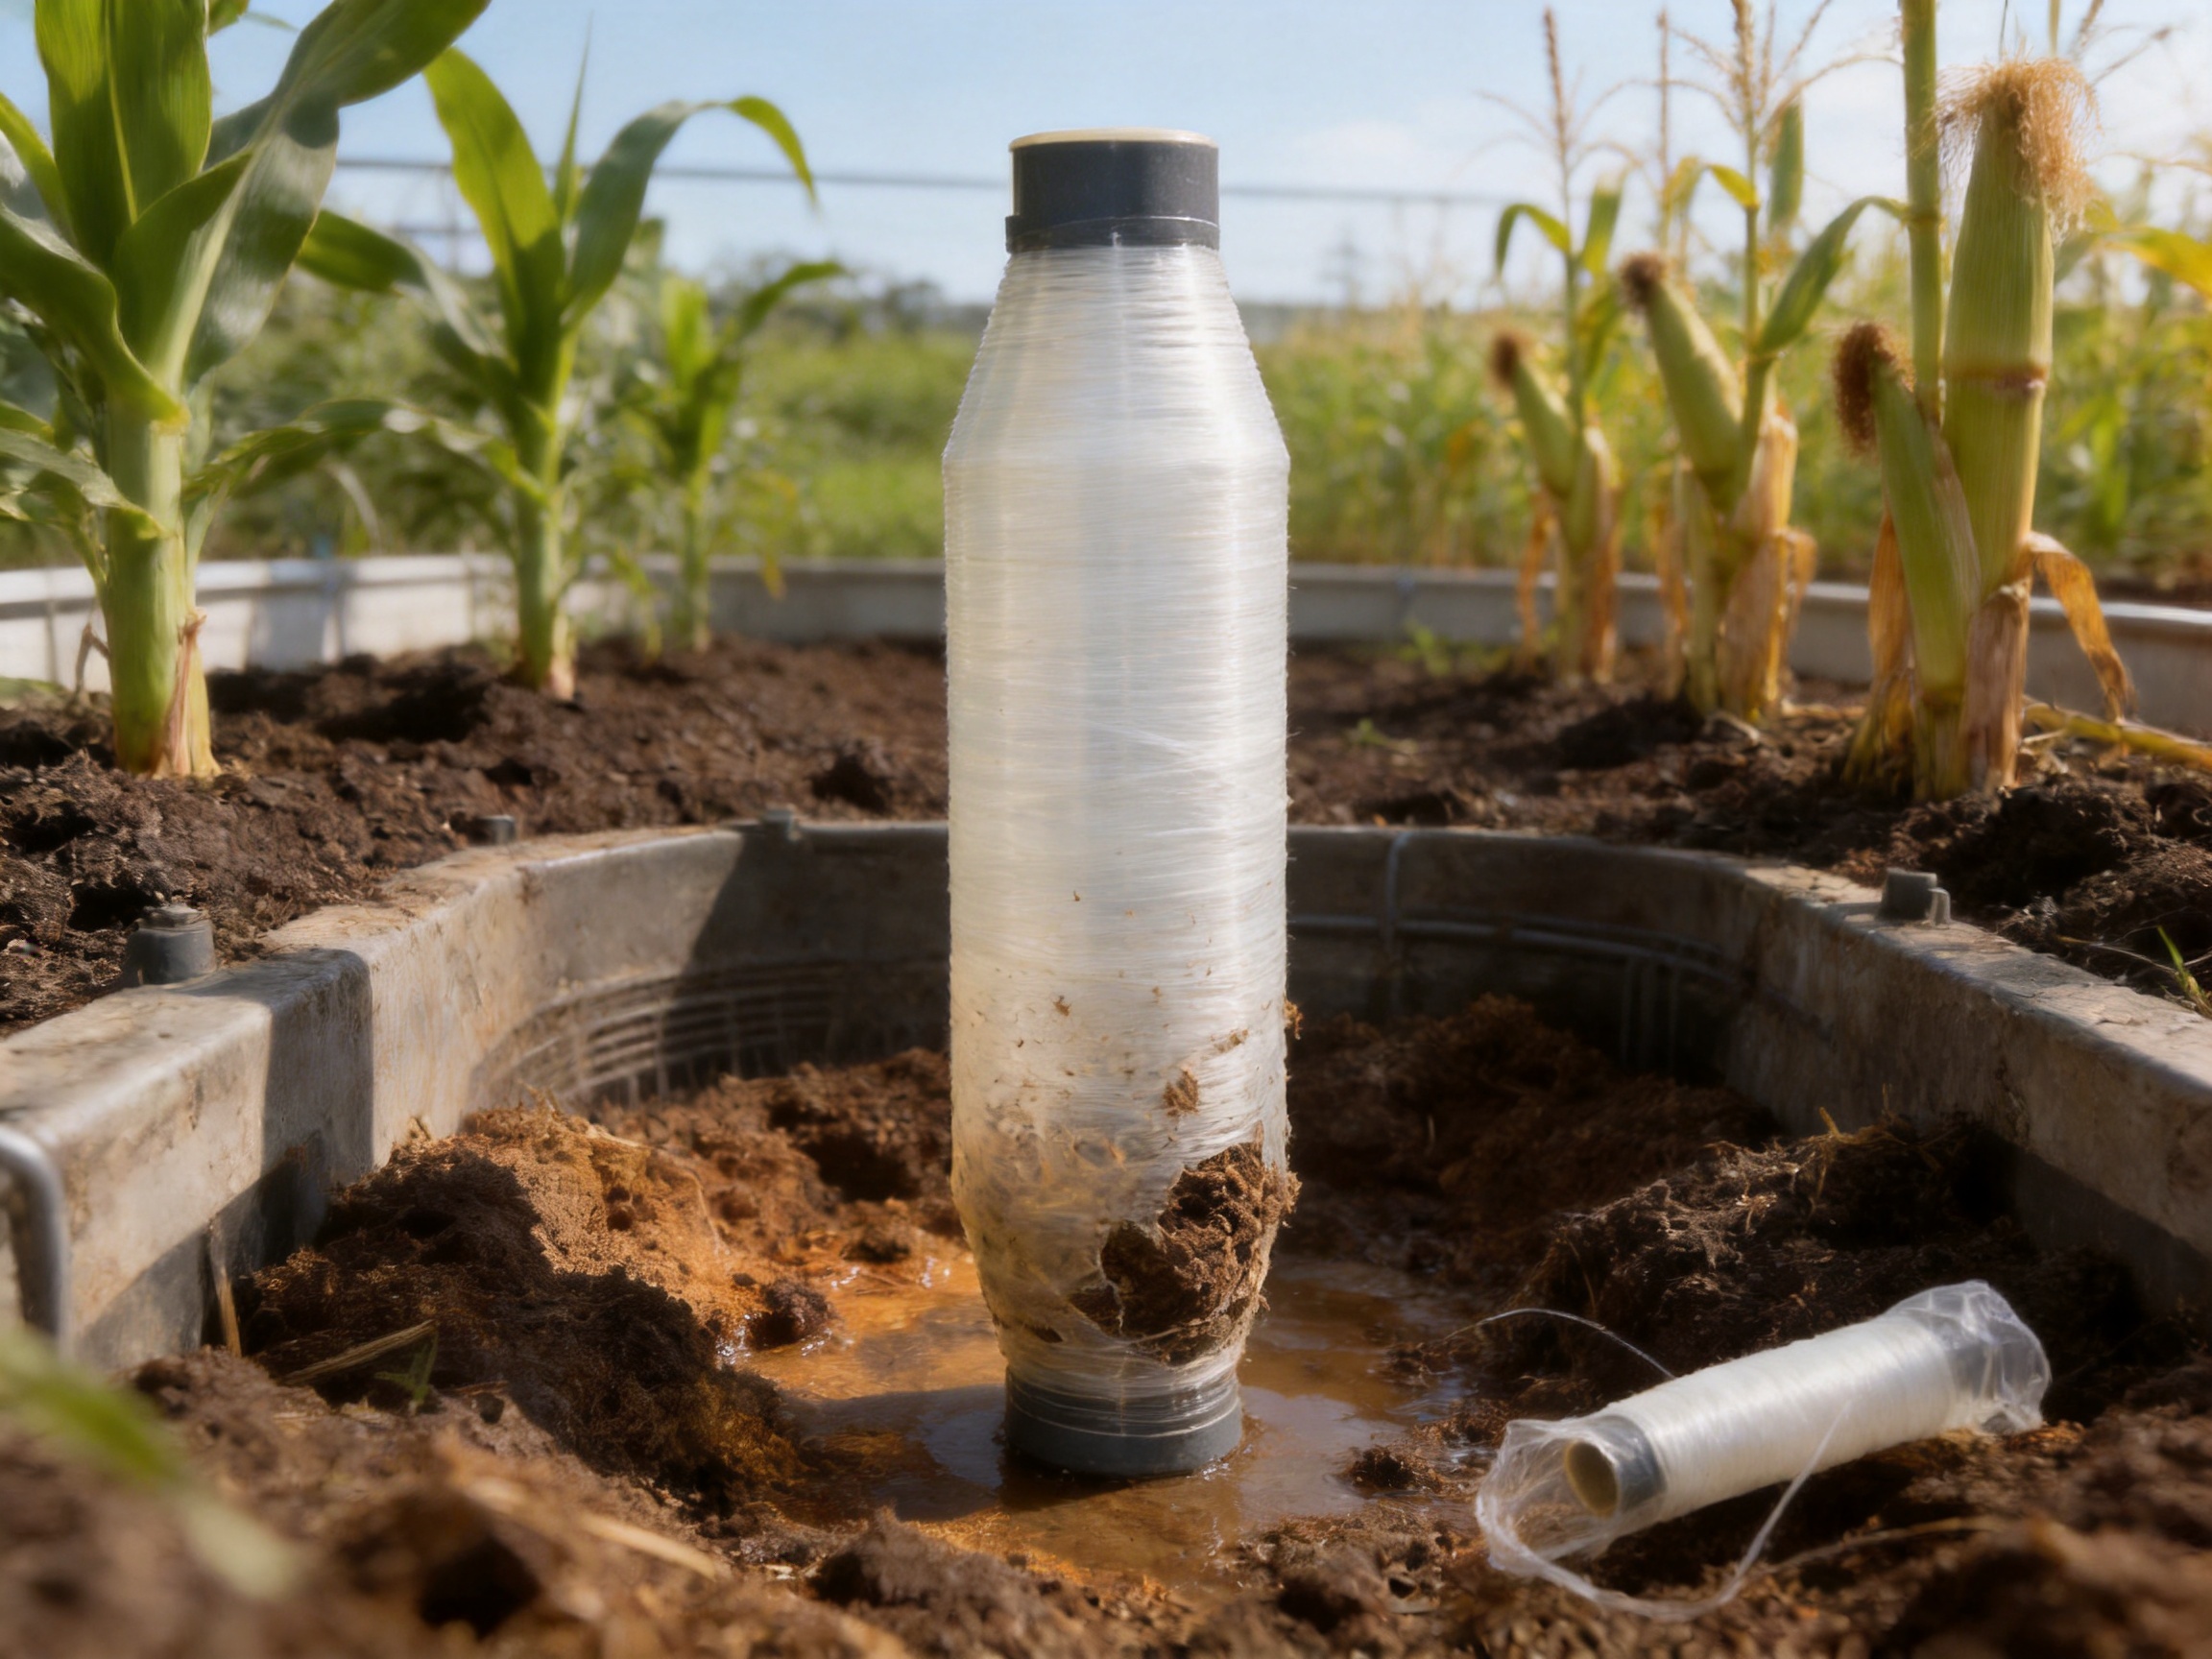
PLA is often described as a material that comes from the earth and can return to the earth under suitable controlled conditions. This statement should be understood accurately. Industrially compostable PLA does not necessarily decompose rapidly in an ordinary home compost bin, landfill, dry soil, or marine environment. It requires the temperature, humidity, microbial activity, and processing time available in a commercial composting facility.
When the appropriate industrial composting conditions are available, PLA can break down into carbon dioxide, water, and biomass. The exact rate depends on filament diameter, crystallinity, additives, composting conditions, and the design of the finished product. For this reason, compostability claims should be supported by product-specific testing and should identify the applicable standard or certification.
From a product development perspective, PLA monofilament is particularly valuable when the final article has a defined service life and can be collected through an industrial composting system. Examples include temporary agricultural netting, selected filtration products, compostable packaging components, and disposable or seasonal textile items.
The yarn is produced from bio-based PLA rather than a conventional fossil-derived polymer. Plant-based sourcing helps brands and manufacturers respond to demand for lower-impact materials, renewable content, and more transparent environmental positioning.
PLA monofilament is intended for industrial composting conditions rather than ordinary household composting. Under suitable conditions, it can disintegrate and biodegrade within a controlled period. Finished products should be evaluated as complete systems because dyes, coatings, additives, reinforcements, and assembly methods can affect compostability.
The monofilament construction provides a smooth and continuous surface. Uniform diameter is important for screen production, netting, weaving, knitting, brush bristles, tea bag strings, and other applications where variations in filament size can affect appearance, tension, filtration accuracy, or machine efficiency.
Standard-grade PLA monofilament can deliver useful tensile strength and controlled elongation for many technical applications. Typical reference values may fall within a tensile strength range of approximately 3.0 to 5.5 grams per denier and an elongation-at-break range of approximately 15 to 35 percent, depending on resin grade, diameter, orientation, drawing conditions, and testing method.
PLA has a lower melting range than many conventional engineering polymers. A typical melting range is approximately 150 to 170 degrees Celsius, although the exact processing window depends on polymer grade and formulation. Lower processing temperatures can support energy-conscious production and may be beneficial when the yarn is incorporated into temperature-sensitive structures.
PLA generally has low moisture regain, commonly below one percent under standard conditions. This feature helps the yarn maintain a relatively dry feel and stable mass during normal storage and use. However, PLA can be vulnerable to hydrolysis when exposed to heat and moisture simultaneously, so careful drying and storage remain important.
The product is promoted for anti-bacterial performance and resistance to mold growth. The actual performance depends on polymer grade, surface condition, processing, environmental exposure, and test method. For applications requiring an antimicrobial claim, the finished yarn or finished article should be tested according to the relevant national or international standard.
PLA monofilament can provide useful UV stability for selected outdoor and agricultural applications. UV performance varies according to filament orientation, stabilizer package, color, exposure intensity, temperature, and duration. Additive treatment can improve resistance where a longer outdoor service life is required.
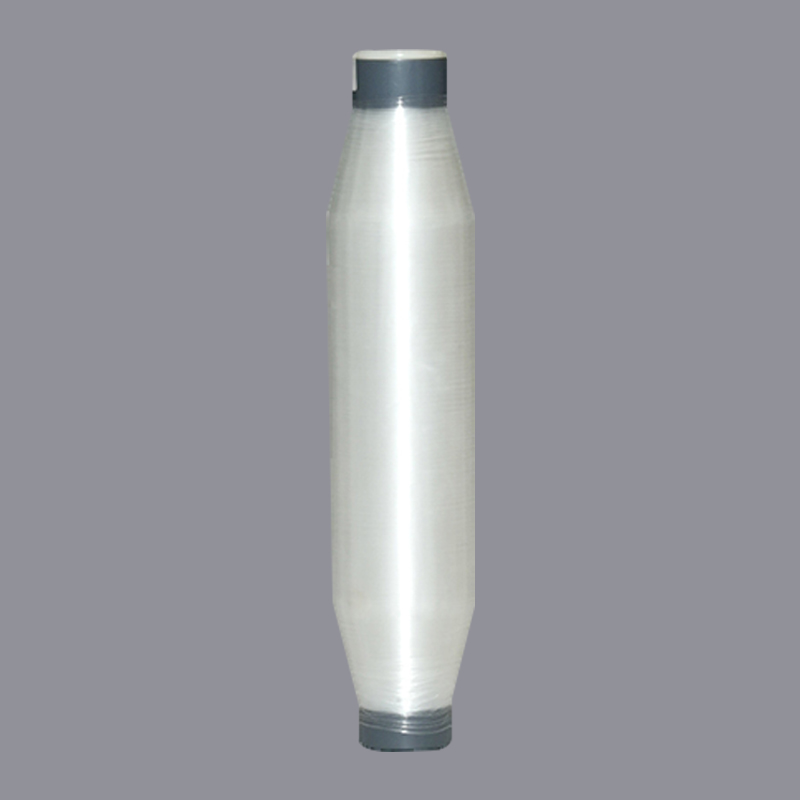
PLA Biodegradable Monofilament Yarn
The quality of biodegradable monofilament depends not only on the PLA resin but also on the precision of the production process. A technically capable manufacturer must control raw materials, melt processing, extrusion, drawing, heat setting, winding, inspection, and packaging as an integrated system.
Production begins with the selection of an appropriate PLA resin. Resin selection considers melt flow behavior, molecular weight, optical requirements, melting range, toughness, crystallization behavior, biodegradation objectives, and intended application. A yarn designed for weaving may require a different balance of stiffness and elongation than a filament designed for filtration or agricultural netting.
Incoming resin should be checked for packaging integrity, batch identity, moisture condition, and material consistency. PLA is sensitive to moisture during melt processing. If water is present in the polymer and the material is heated, hydrolysis can reduce molecular weight and weaken the final filament. Proper storage and pre-drying are therefore important parts of a reliable production system.
Before extrusion, the resin is dried under controlled conditions. The objective is to remove absorbed moisture without causing premature thermal aging. Drying temperature, time, airflow, and dew point must be controlled according to the selected PLA grade.
Consistent drying helps maintain stable melt viscosity. Stable viscosity supports steady extrusion pressure, more consistent filament diameter, and improved tensile performance. It also reduces the risk of bubbles, surface defects, brittleness, and unexpected breaks during drawing or downstream processing.
In the extrusion stage, dried PLA pellets are conveyed into a heated extruder. The screw gradually melts and homogenizes the resin. Temperature zones are carefully managed so that the polymer reaches a uniform melt state without excessive residence time or thermal degradation.
Stable pressure and mixing are essential. Excessive shear or overheating may damage the polymer, while insufficient melting can create unmelted particles and surface irregularities. A professional extrusion process uses controlled temperature profiles, consistent feeding, and suitable filtration to produce a clean and homogeneous melt.
The spinneret determines the basic geometry of the filament as it leaves the extrusion head. For monofilament production, spinneret design must support a round and consistent cross-section. The condition of the spinneret, the accuracy of its orifice, and the pressure stability of the melt all influence the final diameter.
Diameter consistency is particularly important for filtration mesh, woven screens, agricultural nets, and precision textile structures. Even small variations can change opening size, tension distribution, handle, or machine settings. Regular inspection and maintenance of the spinneret and extrusion system help protect product consistency.
After leaving the spinneret, the molten filament passes through a controlled cooling zone. Cooling may be achieved through air, water, or a combination of process methods, depending on the product design and equipment configuration.
Cooling affects crystallization, surface quality, stiffness, and dimensional stability. If the filament cools too quickly or unevenly, internal stress and diameter variation may develop. If cooling is too slow, the filament may remain soft for too long and become difficult to draw or guide. Optimized cooling conditions help create a stable foundation for the subsequent orientation process.
Drawing stretches the solidified filament under controlled tension. This process orients polymer chains along the filament axis and improves tensile performance, dimensional stability, and handling characteristics. The draw ratio must be matched to the PLA grade, filament diameter, target elongation, and intended application.
Over-drawing may make the filament excessively brittle, while under-drawing may result in insufficient strength or poor dimensional control. The production team therefore balances strength, flexibility, elongation, and resistance to breakage. This balance is essential because a yarn for high-tension weaving may require different properties from a yarn used in a soft knitted construction.
Heat setting can be used to stabilize the molecular structure after drawing. Controlled thermal treatment reduces internal stress and improves dimensional stability during later processing. The treatment must remain within the thermal limits of PLA to prevent degradation or unwanted deformation.
Appropriate relaxation control can also reduce shrinkage during weaving, knitting, dyeing, or subsequent heat exposure. This is especially important for technical applications that require consistent mesh dimensions or stable finished-product geometry.
After the filament has been formed and stabilized, it is wound onto packages suitable for transport and downstream processing. Winding tension must be controlled carefully. Excessive tension can deform the package or influence unwinding behavior, while insufficient tension can create loose layers, slippage, or tangling.
A well-formed package helps customers achieve smoother unwinding, fewer machine interruptions, and better production efficiency. Package size, core type, labeling, and winding format can be adjusted according to customer requirements.
Quality control may include online diameter monitoring, visual surface inspection, tensile testing, elongation testing, denier verification, moisture checks, color evaluation, and package inspection. Testing frequency depends on the product specification and customer requirements.
Important control points include raw material identity, moisture condition, melt stability, filament diameter, linear density, tensile strength, elongation, appearance, winding quality, and lot traceability. Maintaining production records allows deviations to be investigated and supports consistent repeat orders.
The following values are general reference ranges for standard PLA monofilament yarn. Actual results may vary according to count, diameter, polymer grade, additives, drawing ratio, test method, and production conditions. Customers should request a product-specific technical data sheet before final approval.
| Property | Typical Reference | Importance in Application |
| Polymer | Polylactic acid derived from renewable plant resources | Provides bio-based content and a compostability pathway |
| Available standard count | 30D | Suitable for selected textile and specialty filament applications |
| Diameter range | Approximately 0.05 to 3.0 mm, depending on design | Allows adaptation to textile, mesh, filtration, and technical uses |
| Tensile strength | Approximately 3.0 to 5.5 grams per denier | Supports tension-bearing and structural applications |
| Elongation at break | Approximately 15 to 35 percent | Influences flexibility, impact response, and processability |
| Melting point | Approximately 150 to 170 degrees Celsius | Guides heat-processing and dyeing conditions |
| Density | Approximately 1.24 to 1.27 grams per cubic centimeter | Affects weight, coverage, and finished-product calculations |
| Moisture regain | Generally below 1 percent | Supports low moisture absorption during normal use |
| UV stability | Moderate, with improvement possible through additives | Relevant to agricultural and outdoor products |
The most visible distinction between PLA and conventional polyester or nylon monofilament is the source of the polymer. PLA can be manufactured from renewable plant-based feedstocks, while conventional alternatives are generally linked to fossil resources. This makes PLA attractive to companies working toward renewable-material targets or improved environmental reporting.
When correctly designed, collected, and processed, PLA products can be directed toward industrial composting at the end of their useful life. Conventional monofilaments generally remain persistent for a much longer period and may require mechanical recycling, chemical recycling, incineration, or landfill disposal.
Industrial compostability does not eliminate the need for responsible waste management. A PLA product that enters the wrong waste stream may not receive the conditions required for degradation. Nevertheless, where collection and composting infrastructure are available, PLA can offer an end-of-life option that conventional monofilament does not provide.
PLA typically melts at a lower temperature than many nylon and polyester grades. This can provide advantages in selected low-temperature processing applications and may reduce the thermal load on associated materials. It can also support processing systems designed around moderate heat exposure.
The lower heat resistance is also a limitation. PLA should not automatically replace conventional monofilament in high-temperature environments. Product designers must evaluate service temperature, hot-water exposure, ironing, heat sealing, sterilization, and other thermal conditions before selecting the material.
Products made from PLA can support sustainability-oriented branding when claims are accurate, documented, and connected to the final product. Renewable content, industrial compostability, and reduced dependence on fossil-based polymers can be meaningful advantages in consumer goods, packaging, agriculture, and textile markets.
PLA monofilament is not intended to outperform every nylon or polyester product in every category. Conventional materials may offer higher heat resistance, broader chemical resistance, longer outdoor durability, or lower cost. PLA's competitive strength is its balance: it provides useful technical performance while supporting renewable sourcing and a controlled biodegradation pathway.
| Evaluation Factor | PLA Monofilament | Conventional Nylon or Polyester Monofilament |
| Feedstock | Renewable plant-based resources may be used | Generally fossil-based resources |
| End-of-life option | Industrial composting under suitable conditions | Usually long-term persistence, recycling, or disposal |
| Heat resistance | Lower and application-dependent | Often higher, depending on polymer grade |
| Moisture behavior | Low moisture regain but sensitive to hydrolysis during hot, wet processing | Varies by polymer; nylon can absorb more moisture |
| UV performance | Moderate and improvable with stabilizers | Varies widely and may also require stabilization |
| Environmental positioning | Renewable and industrially compostable potential | Established performance with fewer compostability options |
| Cost structure | May be higher because of resin and processing economics | Often lower due to mature supply chains |
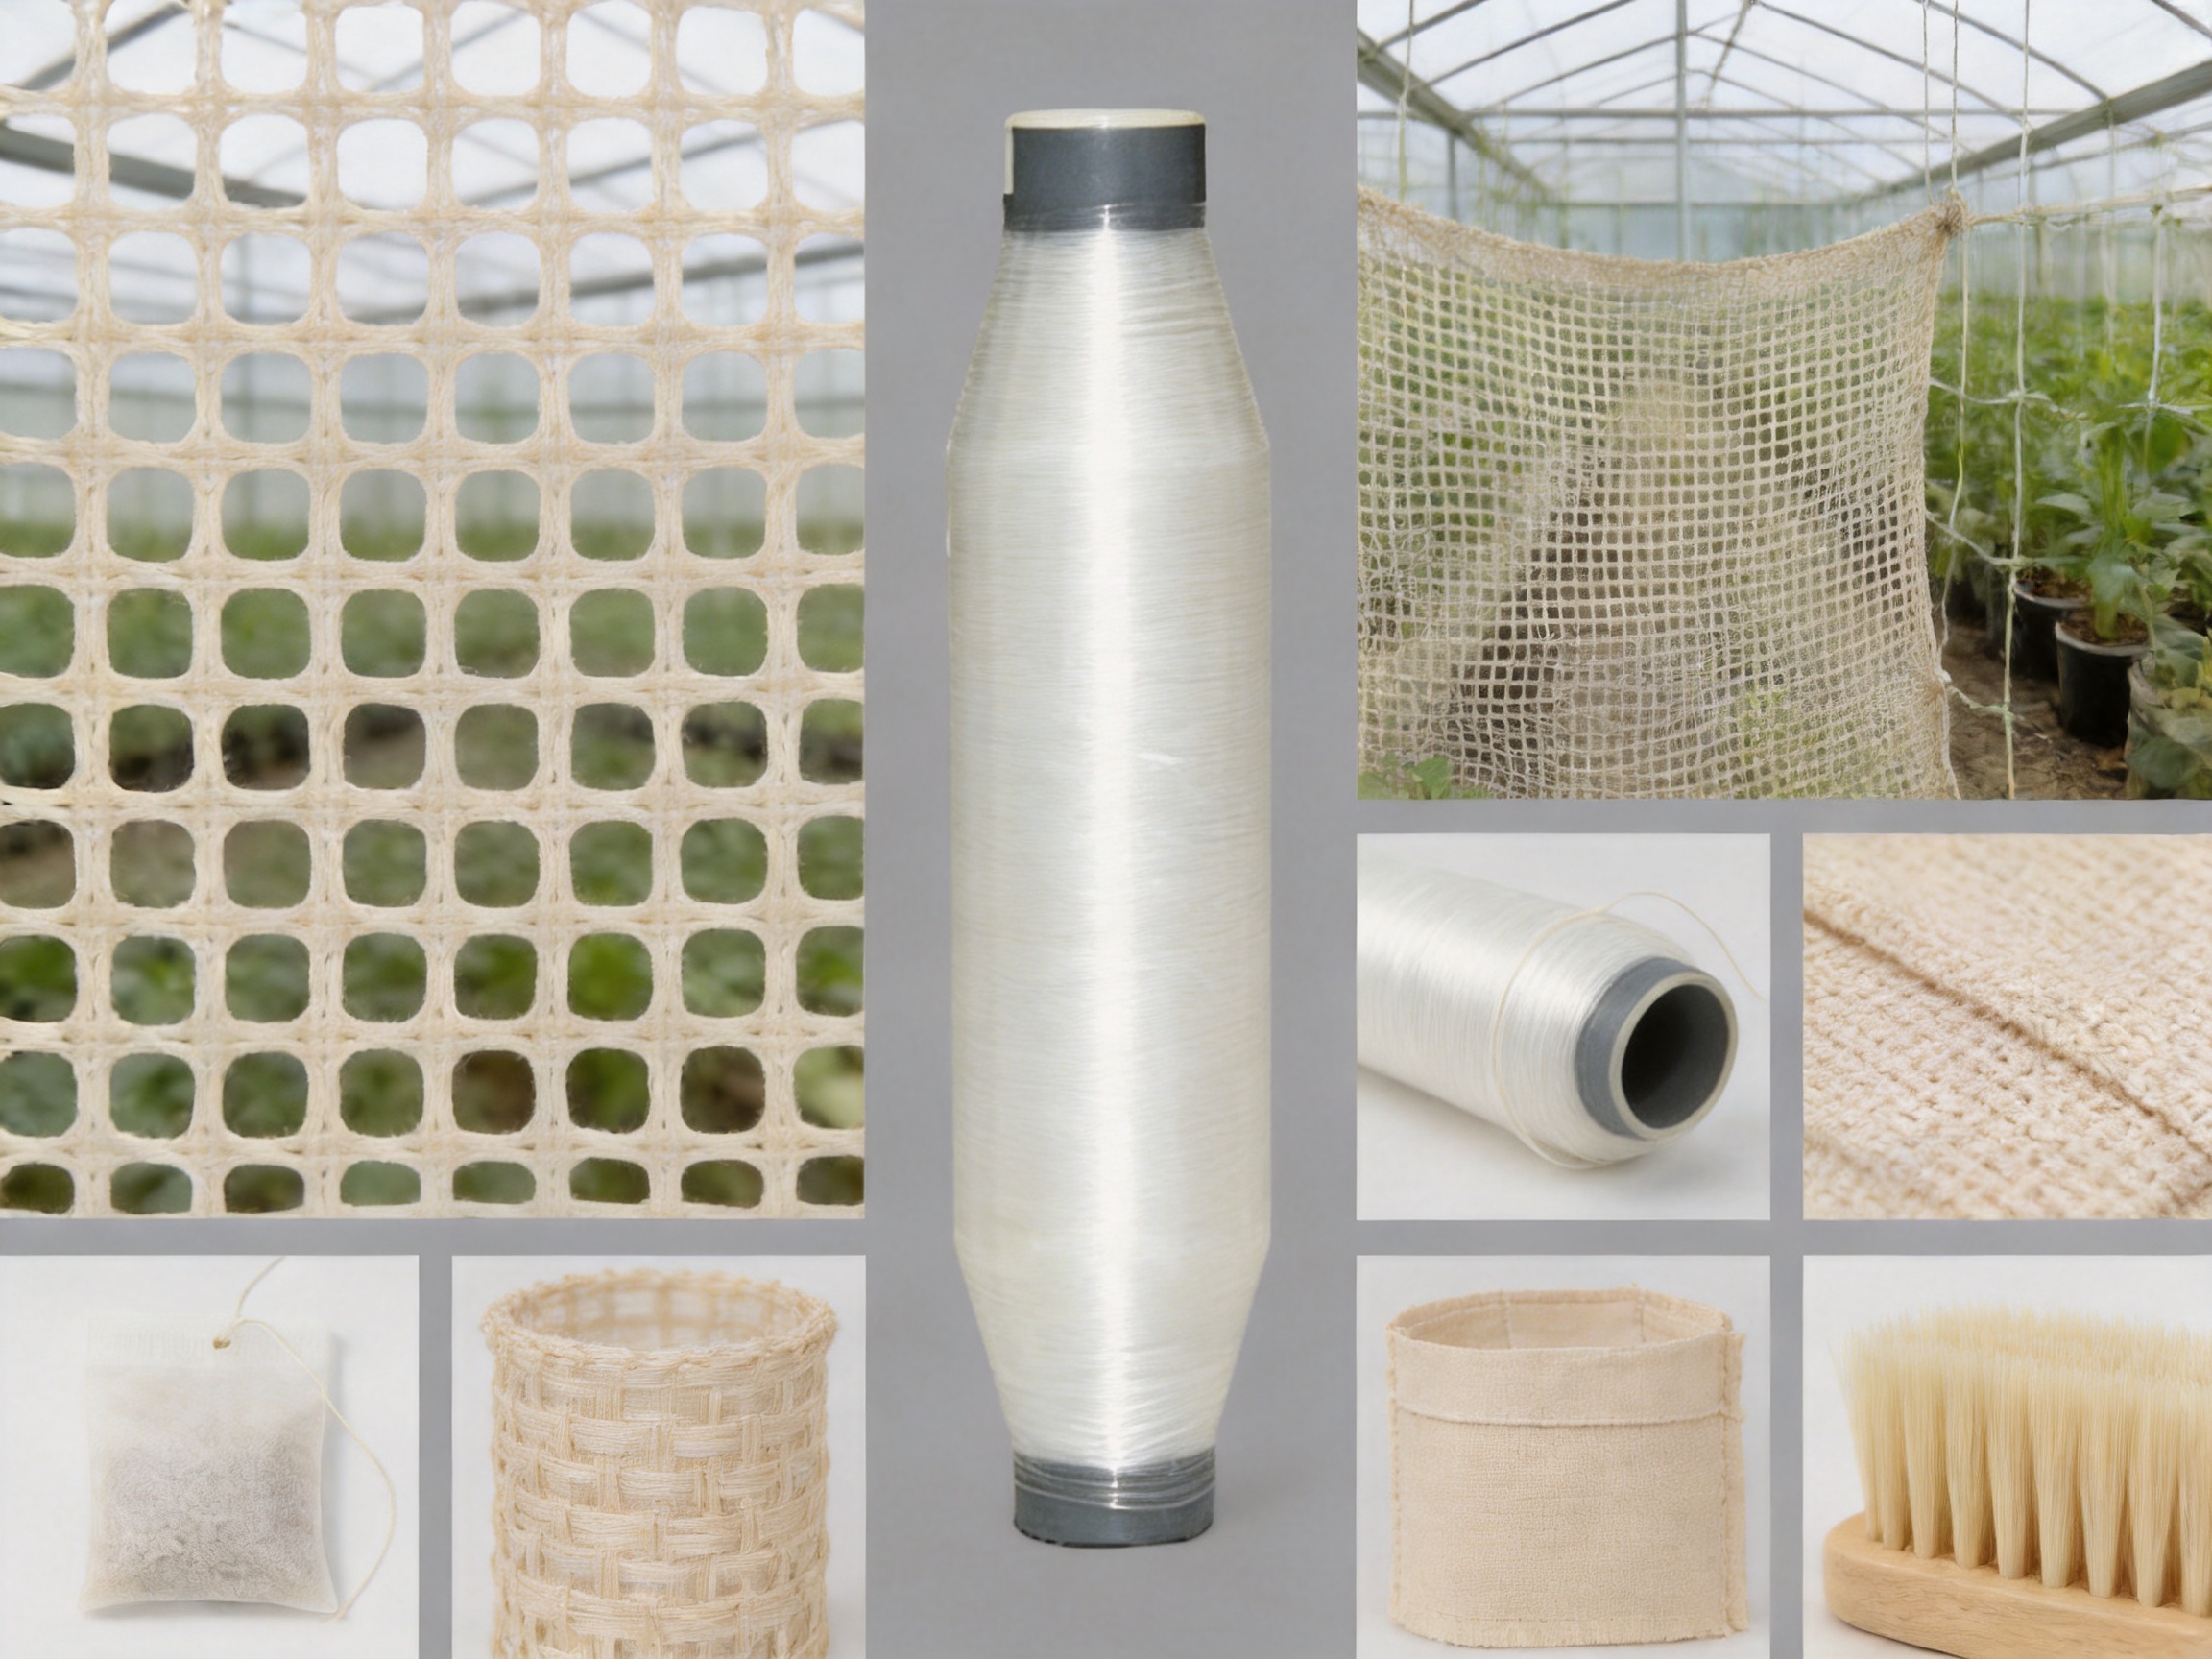
PLA monofilament can be used in biodegradable filter mesh, temporary screens, flour sifting structures, and selected liquid filtration bags. The smooth surface and consistent diameter support predictable mesh openings and straightforward cleaning during production.
Filtration designers should consider chemical compatibility, temperature, pressure, particle size, and the required service period. PLA is most suitable where the filtration process operates within its thermal and chemical limits and where the end product can be recovered for industrial composting.
Agricultural applications are one of the most promising areas for biodegradable monofilament. The yarn can be incorporated into crop support lines, greenhouse shading structures, trellising systems, crop nets, erosion-control fabrics, and temporary horticultural materials.
After the growing season, selected products may be collected or incorporated into an approved composting or soil-management program, depending on local regulations and product design. PLA is especially attractive where removing conventional plastic netting from fields is costly or difficult.
Outdoor performance must be evaluated carefully. Sunlight, rain, temperature cycling, fertilizers, pesticides, and mechanical abrasion can influence service life. UV stabilizers and suitable product construction may be necessary when the material is expected to remain outdoors for an extended period.
The yarn can be used for tea bag strings and other specialty food-related textile components when the complete construction complies with applicable food-contact requirements. Its renewable origin can support sustainable packaging programs, while its smooth monofilament structure provides clean handling and consistent appearance.
Food-contact suitability should never be assumed solely from the use of PLA. Resin additives, colorants, finishes, lubricants, and processing aids must be evaluated for the intended regulatory market.
PLA monofilament can be introduced into woven or knitted textiles where designers want a distinctive structure, controlled stiffness, or renewable-content story. It can be used alone or combined with other fibers to create dimensional effects, mesh constructions, decorative surfaces, or technical fabrics.
Because PLA has a different melting range and dyeing behavior from polyester, textile mills should optimize machine settings, heat exposure, dye chemistry, and finishing conditions. Trial production is recommended before commercial-scale conversion.
The smooth and continuous structure of monofilament makes it suitable for selected brush bristles and specialty cleaning products. PLA-based bristles may be considered for products where moderate stiffness, renewable sourcing, and a defined service life are important.
Brush developers should test bending recovery, fatigue, abrasion resistance, water exposure, chemical compatibility, and end-of-life behavior in the final brush design.
PLA monofilament can support compostable packaging systems as string, mesh, tie material, reinforcement, or structural components. It may be used where the packaging requires additional tensile support but must maintain a renewable or compostable material profile.
The entire packaging system should be evaluated. A compostable filament cannot make a package compostable if other components, coatings, inks, adhesives, or labels prevent the finished product from meeting the applicable requirements.
PLA is widely recognized as a useful material for additive manufacturing. Monofilament or filament formats can be considered for selected prototyping, modeling, and specialty extrusion applications. Processing temperature, diameter tolerance, cooling, and adhesion must be adapted to the equipment.
For demanding engineering applications, users should evaluate heat distortion, impact strength, layer adhesion, moisture exposure, and dimensional accuracy. Standard PLA is generally better suited to moderate-temperature applications than to high-temperature engineering parts.
As a special textile manufacturer, GC FIBER focuses on functional and eco-friendly yarn products, including biodegradable yarn, low melting yarn, ECDP yarn, anti-static yarn, HDPE yarn, bio-component yarn, and polyester filament yarn. This product range provides experience across different polymer systems and application requirements.
Experience with multiple functional yarn categories is valuable because PLA monofilament production requires a combination of polymer knowledge, extrusion control, textile understanding, and application development. A manufacturer that understands only commodity yarn may not provide the same level of support when customers need customized counts, special dimensions, compound formulations, or new material structures.
The manufacturing process can be adapted around the customer's finished-product requirements. Important development questions include the desired denier, diameter, stiffness, elongation, color, package size, application temperature, outdoor exposure, compostability target, and downstream machinery.
By discussing the final use before production, the yarn specification can be matched more effectively to the application. For example, a filtration mesh may prioritize diameter uniformity and stiffness, while a textile application may require improved flexibility and dye acceptance. Agricultural products may require a different balance of UV stability, tensile strength, and controlled service life.
The standard product information lists 30D as an available count, while special production can be arranged by order. Custom production may involve adjustments to count, filament diameter, color, finish, package format, or performance objectives, subject to technical feasibility and minimum order requirements.
Special orders should be confirmed through sample approval and technical documentation. A clear specification reduces misunderstandings and helps ensure that trial material, bulk production, and repeat orders remain aligned.
PLA yarn performance depends heavily on conversion conditions. Technical support is therefore important beyond the delivery of the yarn itself. Customers may need guidance on drying, storage, heat exposure, dyeing, winding tension, loom settings, knitting conditions, or compostability communication.
GC FIBER's focus on special and functional textile materials allows it to cooperate with customers developing new materials. This cooperation can be especially useful for businesses moving from a conventional polymer to a bio-based alternative and requiring several rounds of trial production.
Traceability is important for technical yarn. Resin batch, production date, specification, package number, and inspection results should be recorded so that quality trends can be reviewed. Traceability also supports customer complaint analysis and the consistent reproduction of approved material.
The product is supplied from China, with Shanghai seaport listed as the shipping port. Export packaging should protect the yarn from moisture, contamination, compression, and excessive temperature fluctuation during transportation. Because PLA is sensitive to hydrolysis and premature aging, shipping and storage conditions deserve the same attention as production conditions.
PLA monofilament can accept suitable disperse dyes and may also be colored through pigment masterbatching during extrusion. Dye uptake, shade development, color fastness, and heat stability may differ from polyester. Dyeing laboratories should establish the correct temperature, time, carrier, pH, and post-treatment conditions for the selected yarn grade.
Lower dyeing temperatures may be possible compared with some conventional polyester processes. This can reduce thermal exposure and may help protect blended or sensitive materials. However, lower temperature does not automatically guarantee the same shade depth or fastness as a conventional polyester system. Trial dyeing is necessary for commercial color approval.
During weaving and knitting, users should avoid excessive mechanical tension and excessive heat. Machine settings should be adjusted to the yarn's tensile and elongation profile. Guides, needles, reeds, and tension devices should be clean and properly aligned to reduce abrasion and filament breakage.
For extrusion or heat-forming operations, temperature control is critical. PLA should not be held at high temperature for longer than necessary. Excessive heat history may reduce molecular weight, cause discoloration, create odor, or weaken the finished filament.
Correct storage protects both performance and environmental value. A yarn that has been prematurely damaged by moisture, ultraviolet exposure, or overheating may not provide the expected service life and may also become more difficult to process.
Environmental claims must be specific. The terms bio-based, biodegradable, compostable, and industrially compostable do not mean exactly the same thing. Bio-based describes the origin of the carbon or raw material. Biodegradable describes the ability to break down through biological activity under defined or general conditions. Compostable usually refers to biodegradation and disintegration under a particular composting environment and time frame.
ASTM D6400 is commonly referenced in North America for compostable plastics intended for municipal or industrial composting facilities. EN 13432 is widely referenced in Europe for packaging recoverable through industrial composting and biodegradation. These standards involve requirements related to disintegration, biodegradation, ecotoxicity, and material composition.
Testing the raw PLA resin is not always sufficient to validate a finished yarn or finished product. Filament diameter, crystallinity, pigments, additives, coatings, lubricants, and textile construction may change the degradation behavior. The complete product should therefore be tested when a formal claim is required.
Industrial compostability should also be communicated clearly to consumers and waste-management partners. A label that simply says biodegradable may create unrealistic expectations about home composting, marine degradation, or rapid breakdown in soil. Clear instructions improve the likelihood that the material will reach an appropriate recovery route.
PLA monofilament is a strong sustainability option, but it is not suitable for every operating environment. Its heat resistance is lower than that of many conventional engineering fibers. Continuous exposure to high temperatures, hot water, steam, or sterilization may cause dimensional change or loss of strength.
Moisture must also be considered during hot processing. PLA may hydrolyze when heat and moisture are present together. Proper drying, controlled processing, and suitable storage reduce this risk.
Outdoor durability is application-dependent. PLA may perform well in temporary agricultural products, but long-term outdoor exposure can eventually reduce strength because of ultraviolet radiation, moisture, and weathering. Stabilizers, pigments, protective design, and controlled service periods may improve performance.
Chemical resistance should be verified rather than assumed. Acids, alkalis, solvents, oils, detergents, fertilizers, and cleaning agents can interact differently with PLA depending on concentration, temperature, and exposure time.
Finally, industrial compostability requires infrastructure. Before selecting PLA, customers should confirm whether their region has suitable collection and composting channels. If no appropriate end-of-life route exists, the environmental benefit may not be fully realized.
Identify whether the yarn will be used for weaving, knitting, filtration, agriculture, packaging, tea bag strings, brush bristles, or another purpose. Define the required service life, load, temperature, humidity, chemical exposure, and appearance.
Confirm count, diameter, tensile strength, elongation, color, package size, surface finish, and tolerance. The standard listed count is 30D, while special production may be considered for qualified requirements.
Run a controlled trial on the actual weaving, knitting, extrusion, or forming equipment. Record machine speed, tension, temperature, breakage rate, appearance, and finished-product dimensions.
Evaluate tensile strength, dimensional stability, abrasion, moisture exposure, UV aging, temperature resistance, chemical resistance, and any antimicrobial performance required by the application.
Determine whether the finished product is intended for industrial composting and whether the complete construction can meet the relevant standard or certification requirements. Include packaging, labels, coatings, dyes, adhesives, and other components in the evaluation.
Once the trial is successful, approve a written specification, sample, color standard, package format, inspection plan, and delivery requirement. This provides a reference for stable mass production and future repeat orders.
It is a continuous single-filament yarn made from polylactic acid, a polymer that can be produced from renewable plant-based resources. It is designed for textile and technical applications requiring a smooth, consistent filament and an industrial compostability pathway.
Not reliably. Most PLA products require the elevated temperature, controlled humidity, microbial activity, and management conditions available in an industrial composting facility. Home composting is usually cooler and less consistent, so breakdown may be slow or incomplete.
The yarn is made from bio-based PLA derived from renewable resources such as corn starch or sugarcane. The exact renewable content and supporting documentation should be confirmed for the selected product grade and production batch.
The listed standard count is 30D. Special production by order may be possible depending on the required count, diameter, color, performance, and order quantity.
Yes. PLA can accept suitable disperse dyes and can also be colored through pigment masterbatching during extrusion. Dye uptake and fastness may differ from polyester, so laboratory trials are recommended before bulk dyeing.
It can be suitable for temporary or seasonal outdoor products such as agricultural netting and crop support structures. The actual service life depends on UV exposure, weather, moisture, mechanical stress, additives, and product design. Long-term outdoor use should be validated through accelerated and real-time testing.
The product is promoted for anti-bacterial and mold-resistance performance. The level of performance depends on the selected polymer, additives, surface condition, and test method. Formal antimicrobial claims should be supported by testing on the relevant yarn or finished product.
The principal advantages are renewable plant-based sourcing, an industrial compostability pathway, low moisture regain, a smooth continuous structure, and a lower processing-temperature range. Nylon and polyester may still be better for some high-temperature, high-durability, or cost-sensitive applications.
The main limitations include lower heat resistance than many conventional technical polymers, sensitivity to hot and humid processing, application-dependent UV durability, and the need for industrial composting infrastructure. Chemical resistance and long-term outdoor performance should also be checked for each application.
Yes. It can be considered for biodegradable filter mesh, flour sifting screens, liquid filtration bags, and other temporary filtration structures. The required mesh opening, pressure, temperature, chemical environment, and service period must be evaluated before selection.
Yes. Potential uses include crop support lines, greenhouse structures, trellising twines, erosion-control fabrics, and temporary crop nets. Outdoor exposure and the desired breakdown time should be considered carefully.
Store it in a cool, dry place away from direct sunlight and moisture. Keep packages sealed until use, avoid hot and humid storage, and use appropriate drying procedures if the yarn has absorbed moisture before processing.
Special production by order is available for qualified requirements. Customers should provide information about count, diameter, color, tensile strength, elongation, package type, application, processing method, and compostability expectations.
The listed shipping location is Shanghai seaport in China. Export packaging and logistics arrangements should be confirmed according to the order quantity, destination, and required delivery schedule.
The customer should request product documentation and, where necessary, conduct testing on the complete finished article. Relevant frameworks may include ASTM D6400 or EN 13432, depending on the target market and product category. Certification requirements should be confirmed before making a regulated environmental claim.
PLA Biodegradable Monofilament Yarn provides a practical route toward more sustainable technical textiles and single-filament products. Its renewable plant-based origin, industrial compostability potential, smooth surface, controlled diameter, useful tensile performance, low moisture regain, and lower processing-temperature range make it a compelling alternative for carefully selected applications.
The product is particularly well suited to agricultural materials, temporary filtration media, compostable packaging structures, tea bag strings, specialty textiles, brush components, and other products where the service life and end-of-life pathway can be clearly defined.
Its advantages are strongest when material selection is combined with responsible engineering. Designers must consider heat, moisture, ultraviolet exposure, chemical contact, mechanical stress, dyeing, storage, and waste-management infrastructure. Compostability claims should be supported by recognized testing and should refer to the complete finished product rather than the polymer alone.
With experience in biodegradable yarn and other functional textile materials, GC FIBER supports the development of application-oriented filament solutions. Its manufacturing approach combines resin preparation, controlled extrusion, precision drawing, heat stabilization, winding, inspection, and custom production. This combination allows customers to evaluate PLA not simply as an environmentally attractive polymer, but as a functional yarn designed for real industrial processing.
For companies seeking to reduce fossil-based material use while maintaining reliable textile performance, PLA monofilament is a valuable material option. The most successful projects will be those that match the yarn specification to the application, validate the finished product through testing, and establish a clear industrial composting route at the end of service life.
ASTM International. Standard Specification for Labeling of Plastics Designed to be Aerobically Composted in Municipal or Industrial Facilities.
European Committee for Standardization. Packaging: Requirements for Packaging Recoverable Through Composting and Biodegradation.
International Organization for Standardization. Textiles: Testing Methods for Linear Density, Tensile Properties, and Dimensional Stability.
European Bioplastics. Technical information on bio-based plastics, biodegradability, and industrial composting.
Association of Plastic Recyclers. Guidance on compostable plastics and end-of-life management.
General technical literature on polylactic acid polymer processing, melt extrusion, fiber drawing, crystallization, and hydrolysis control.
Made of PBS (Polybutylene Succinate), fully biodegradable.Features:1.Home compostable2.Raw material: PBS Polybutylene Su...
READ MOREPlease fill out the form below and our team will contact you as soon as possible.
Addres: No.66 Qiaogang Road, Haian, Nantong City, Jiangsu Province, China
E-mail: service@gcfiber.com admin@gcfiber.com
Copyright ? GC FIBER All Rights Reserved. Eco-Friendly Textile Products Manufacturer Biodegradable Yarn Company