English
 中文简体
Made of PBS (Polybutylene Succinate), fully biodegradable.Features:1.Home compostable2.Raw material: PBS Polybutylene Su...
READ MORE
Content
Pure Nylon Low Melting Yarn with a controlled melting point of approximately 110°C is a specialized thermo-fusible yarn designed to combine bonding performance, softness, and processing reliability. Made from 100% copolyamide nylon, this functional yarn melts or softens within a moderate thermal processing range and then solidifies during cooling, forming bonding points between surrounding fibers, yarns, fabrics, or composite materials.
Unlike conventional sewing threads or ordinary reinforcement yarns, low melting yarn performs two functions in one material. Before thermal activation, it can be handled, rewound, knitted, woven, stitched, or combined with other fibers. After heating, it acts as a distributed solid-state adhesive that bonds selected areas of a textile structure without requiring liquid glue, solvent-based adhesive, or hot melt powder.
The product is available in a broad range of counts, including 20D, 30D, 40D, 50D, 70D, 100D, 150D, 200D, and 300D, subject to production confirmation and application requirements. This range allows manufacturers to select a fine bonding yarn for delicate lace or lingerie components, a medium count for apparel and knitted fabrics, or a heavier construction for ropes, cable protection, industrial textiles, and composite structures.
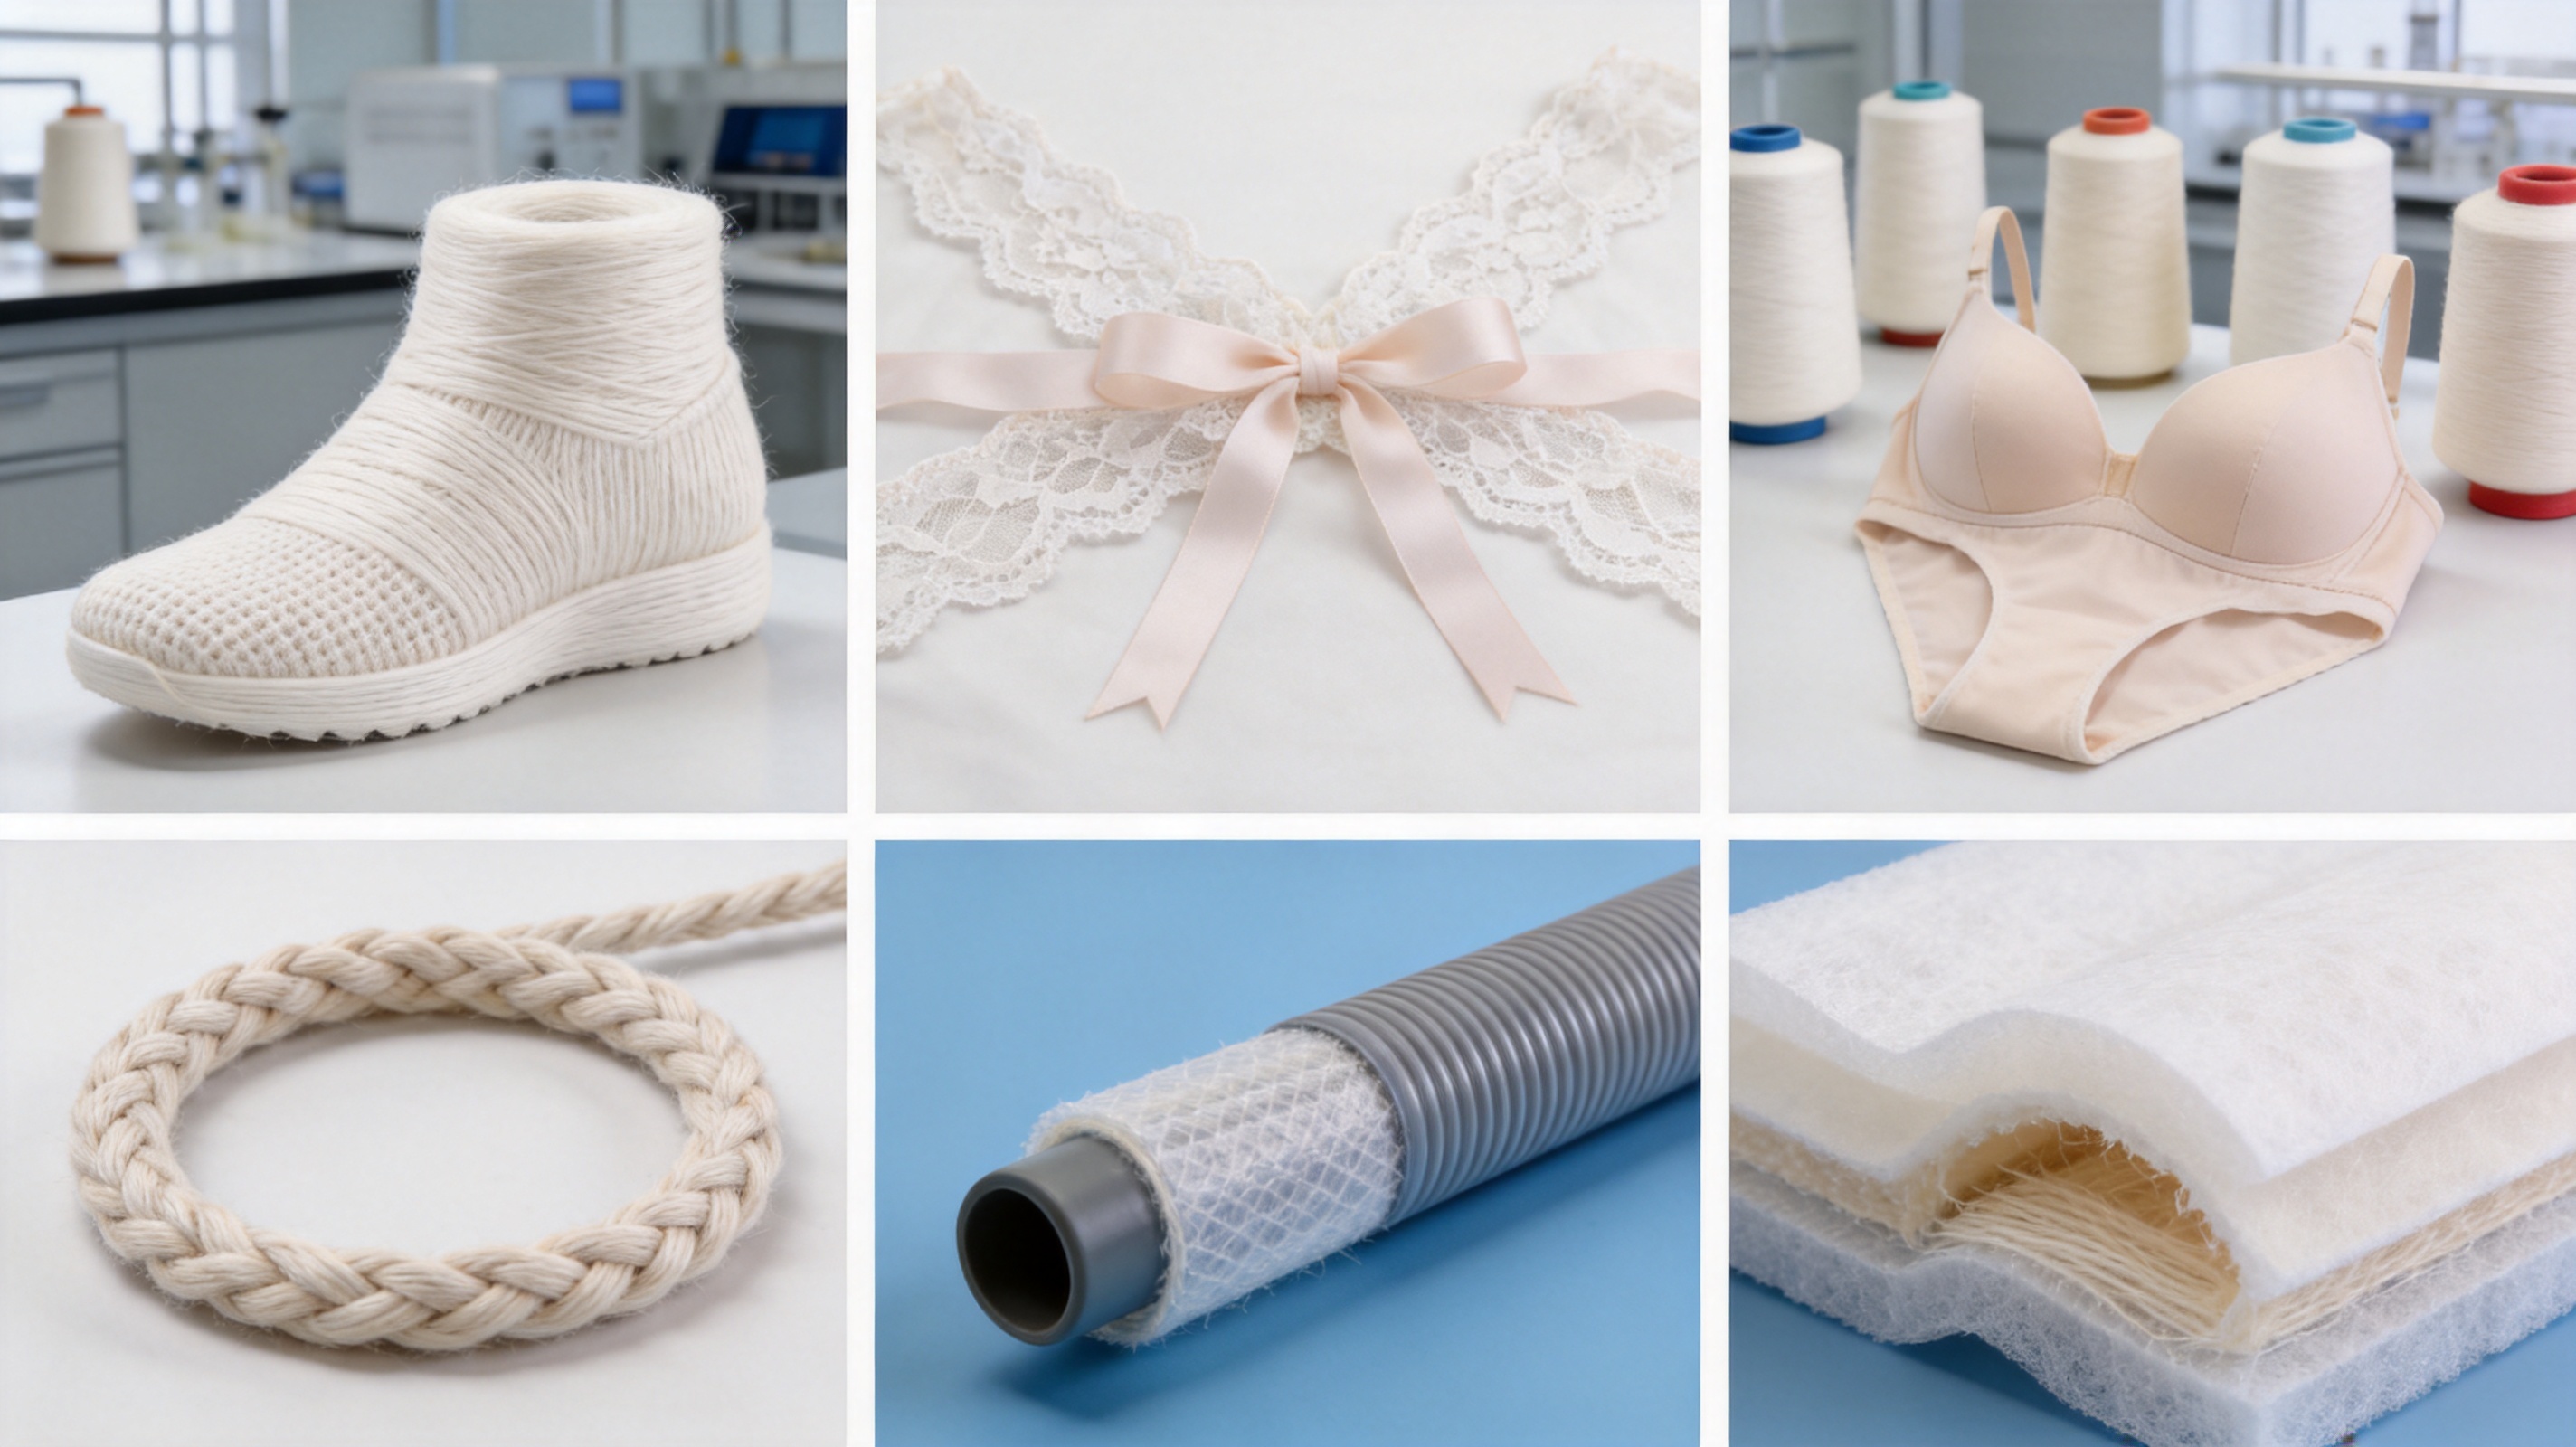
With a soft hand feel, high tenacity, stable thermal behavior, and smooth rewinding performance, 110°C pure nylon low melting yarn is suitable for textile factories that need dependable bonding without sacrificing flexibility or appearance. It can be used in three-dimensional knitted fabrics, chenille yarn, lingerie ribbons, lace, bonded sewing thread, seamless underwear, ropes, cable wire protection, nonwoven composites, interlinings, insulation materials, and other engineered textile products.
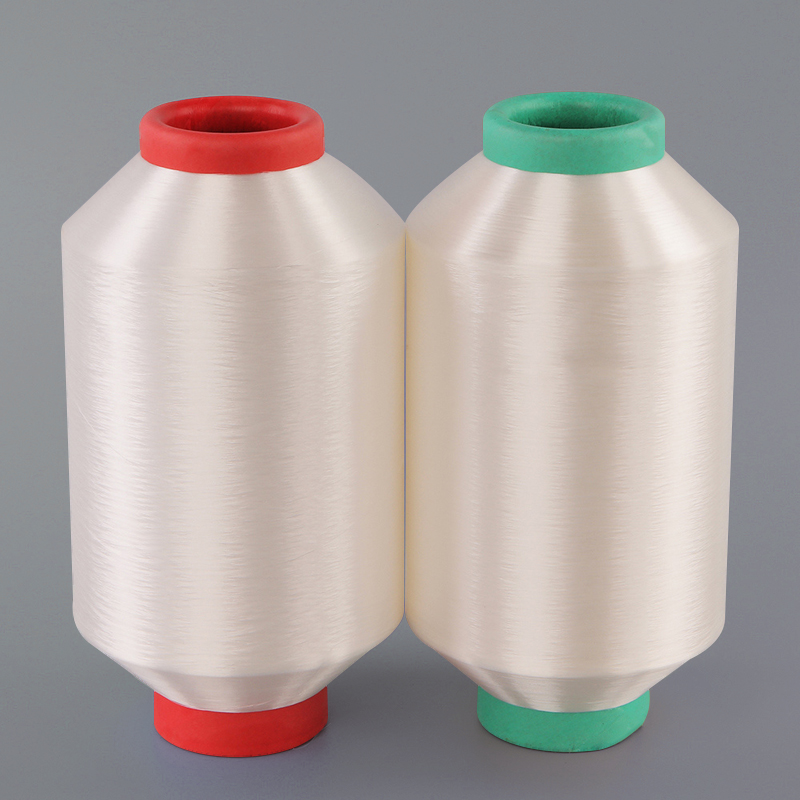
Pure Nylon Low Melting Yarn 110 Degree
Low melting yarn is a functional textile material that contains a polymer designed to soften or melt at a lower temperature than the primary fibers in the surrounding structure. During processing, the yarn remains sufficiently stable for handling and placement. When the material reaches its activation temperature, the low melting component flows into gaps between adjacent fibers or yarns. After cooling, it forms solid bonding points that help hold the structure together.
The 110°C grade described in this article is based on pure nylon or polyamide chemistry. Its bonding behavior is different from that of polyethylene-based or copolyester-based products. The choice of polymer affects the yarn’s hand feel, tenacity, thermal response, flexibility, chemical resistance, washability, and compatibility with the base material.
In practical production, the nominal melting point should not be interpreted as a single mandatory machine setting. A processing window is normally required because the real bonding result depends on the equipment, line speed, pressure, dwell time, fabric thickness, blend ratio, machine calibration, and thermal conductivity of the substrate. A controlled trial is recommended before mass production.
The yarn may be used as a bonding component blended with other fibers, inserted selectively into a knitted or woven construction, wrapped around a core, or applied as a dedicated bonding thread. It can be activated by hot air, a heated roller, a heat press, steam, an industrial oven, or another suitable thermal system. The optimum method depends on the final product and the desired distribution of bonding points.
Pure nylon provides a useful balance between softness and mechanical strength. Many textile applications require a bonding material that can stabilize a structure without making it hard, brittle, noisy, or visibly stiff. Nylon-based low melting yarn can help preserve a comfortable textile hand while improving dimensional stability and resistance to fraying or separation.
The polymer structure also supports high fiber tenacity. This is important before thermal activation because the yarn must withstand unwinding, feeding, knitting, weaving, sewing, needle movement, and other mechanical operations. A low melting yarn that breaks easily during preparation can create production interruptions, uneven bonding, waste, and defects in the finished article.
Another important advantage is compatibility with nylon-rich or flexible textile structures. When the bonding yarn is selected appropriately, the resulting composite can retain a more integrated feel because the bonding material and the surrounding textile have related performance characteristics. This is particularly valuable in close-to-skin garments, lingerie components, sportswear, three-dimensional knitted products, and narrow textile articles.
Pure nylon low melting yarn is also useful where manufacturers want to reduce their dependence on traditional liquid adhesives. Instead of applying glue to the surface, the yarn distributes bonding material through the textile construction. This can improve cleanliness, reduce adhesive handling, and support a more controlled bonding pattern.
The first major advantage is softness. A bonding yarn should reinforce or stabilize the product without creating an unpleasant rigid area. The soft nature of the nylon base helps the final material maintain flexibility, drape, and comfort.
This characteristic is especially important for lingerie ribbon, lace, seamless underwear, elastic narrow fabrics, sports garments, and other products that contact the body. It also benefits footwear uppers and knitted accessories, where excessive stiffness can reduce comfort and impair the ability of the product to flex naturally.
High tenacity supports reliable processing and structural performance. During production, the yarn is exposed to tension, friction, repeated bending, and contact with guides or needles. Improved tensile performance helps reduce yarn breakage and supports more stable operation on automated equipment.
After thermal activation, the bonding points can contribute to the integrity of the finished textile. The final strength depends on the substrate, blend ratio, temperature, pressure, dwell time, and construction, but the yarn is designed to provide both process durability and useful bonding support.
Yarn performance is not determined only by its polymer chemistry. Package quality, winding tension, surface consistency, and handling behavior have a direct effect on production efficiency. A yarn that rewinds smoothly and unwinds evenly is easier to use on high-speed machines.
Controlled winding reduces the risk of loose sections, hard edges, snarling, sloughing, and sudden tension changes. These benefits are relevant to computerized flat knitting machines, automatic sewing equipment, winding machines, braiding equipment, and other systems that require stable yarn delivery.
A controlled melting point of approximately 110°C provides a moderate activation temperature for many textile bonding operations. It can be suitable for facilities using steam setting, heat presses, hot air, calendering, or industrial ovens.
The moderate temperature may also help reduce thermal stress on heat-sensitive base fabrics compared with products that require significantly higher activation temperatures. Nevertheless, every fabric construction should be tested because the acceptable processing temperature is influenced by the most heat-sensitive component in the complete textile system.
After the yarn melts and re-solidifies, the bond can remain flexible rather than forming a completely rigid adhesive layer. This is valuable in applications that must bend, stretch, fold, or recover repeatedly.
Flexible bonding is useful in seamless garments, knitted footwear, cords, composite fabrics, and protective textile structures. It can help reduce peeling, fraying, delamination, or separation while allowing the finished product to retain a degree of movement.
Traditional adhesive systems may require liquid preparation, coating equipment, solvent management, curing control, or additional drying steps. Low melting yarn offers a solid-format alternative that can simplify material handling and reduce the amount of adhesive applied outside the textile structure.
It is important to describe the product accurately: it can reduce or replace chemical adhesives in selected applications, but the degree of replacement must be established through technical trials. Bond strength, wash resistance, fabric compatibility, cost, and production speed all need to be assessed before a full conversion.
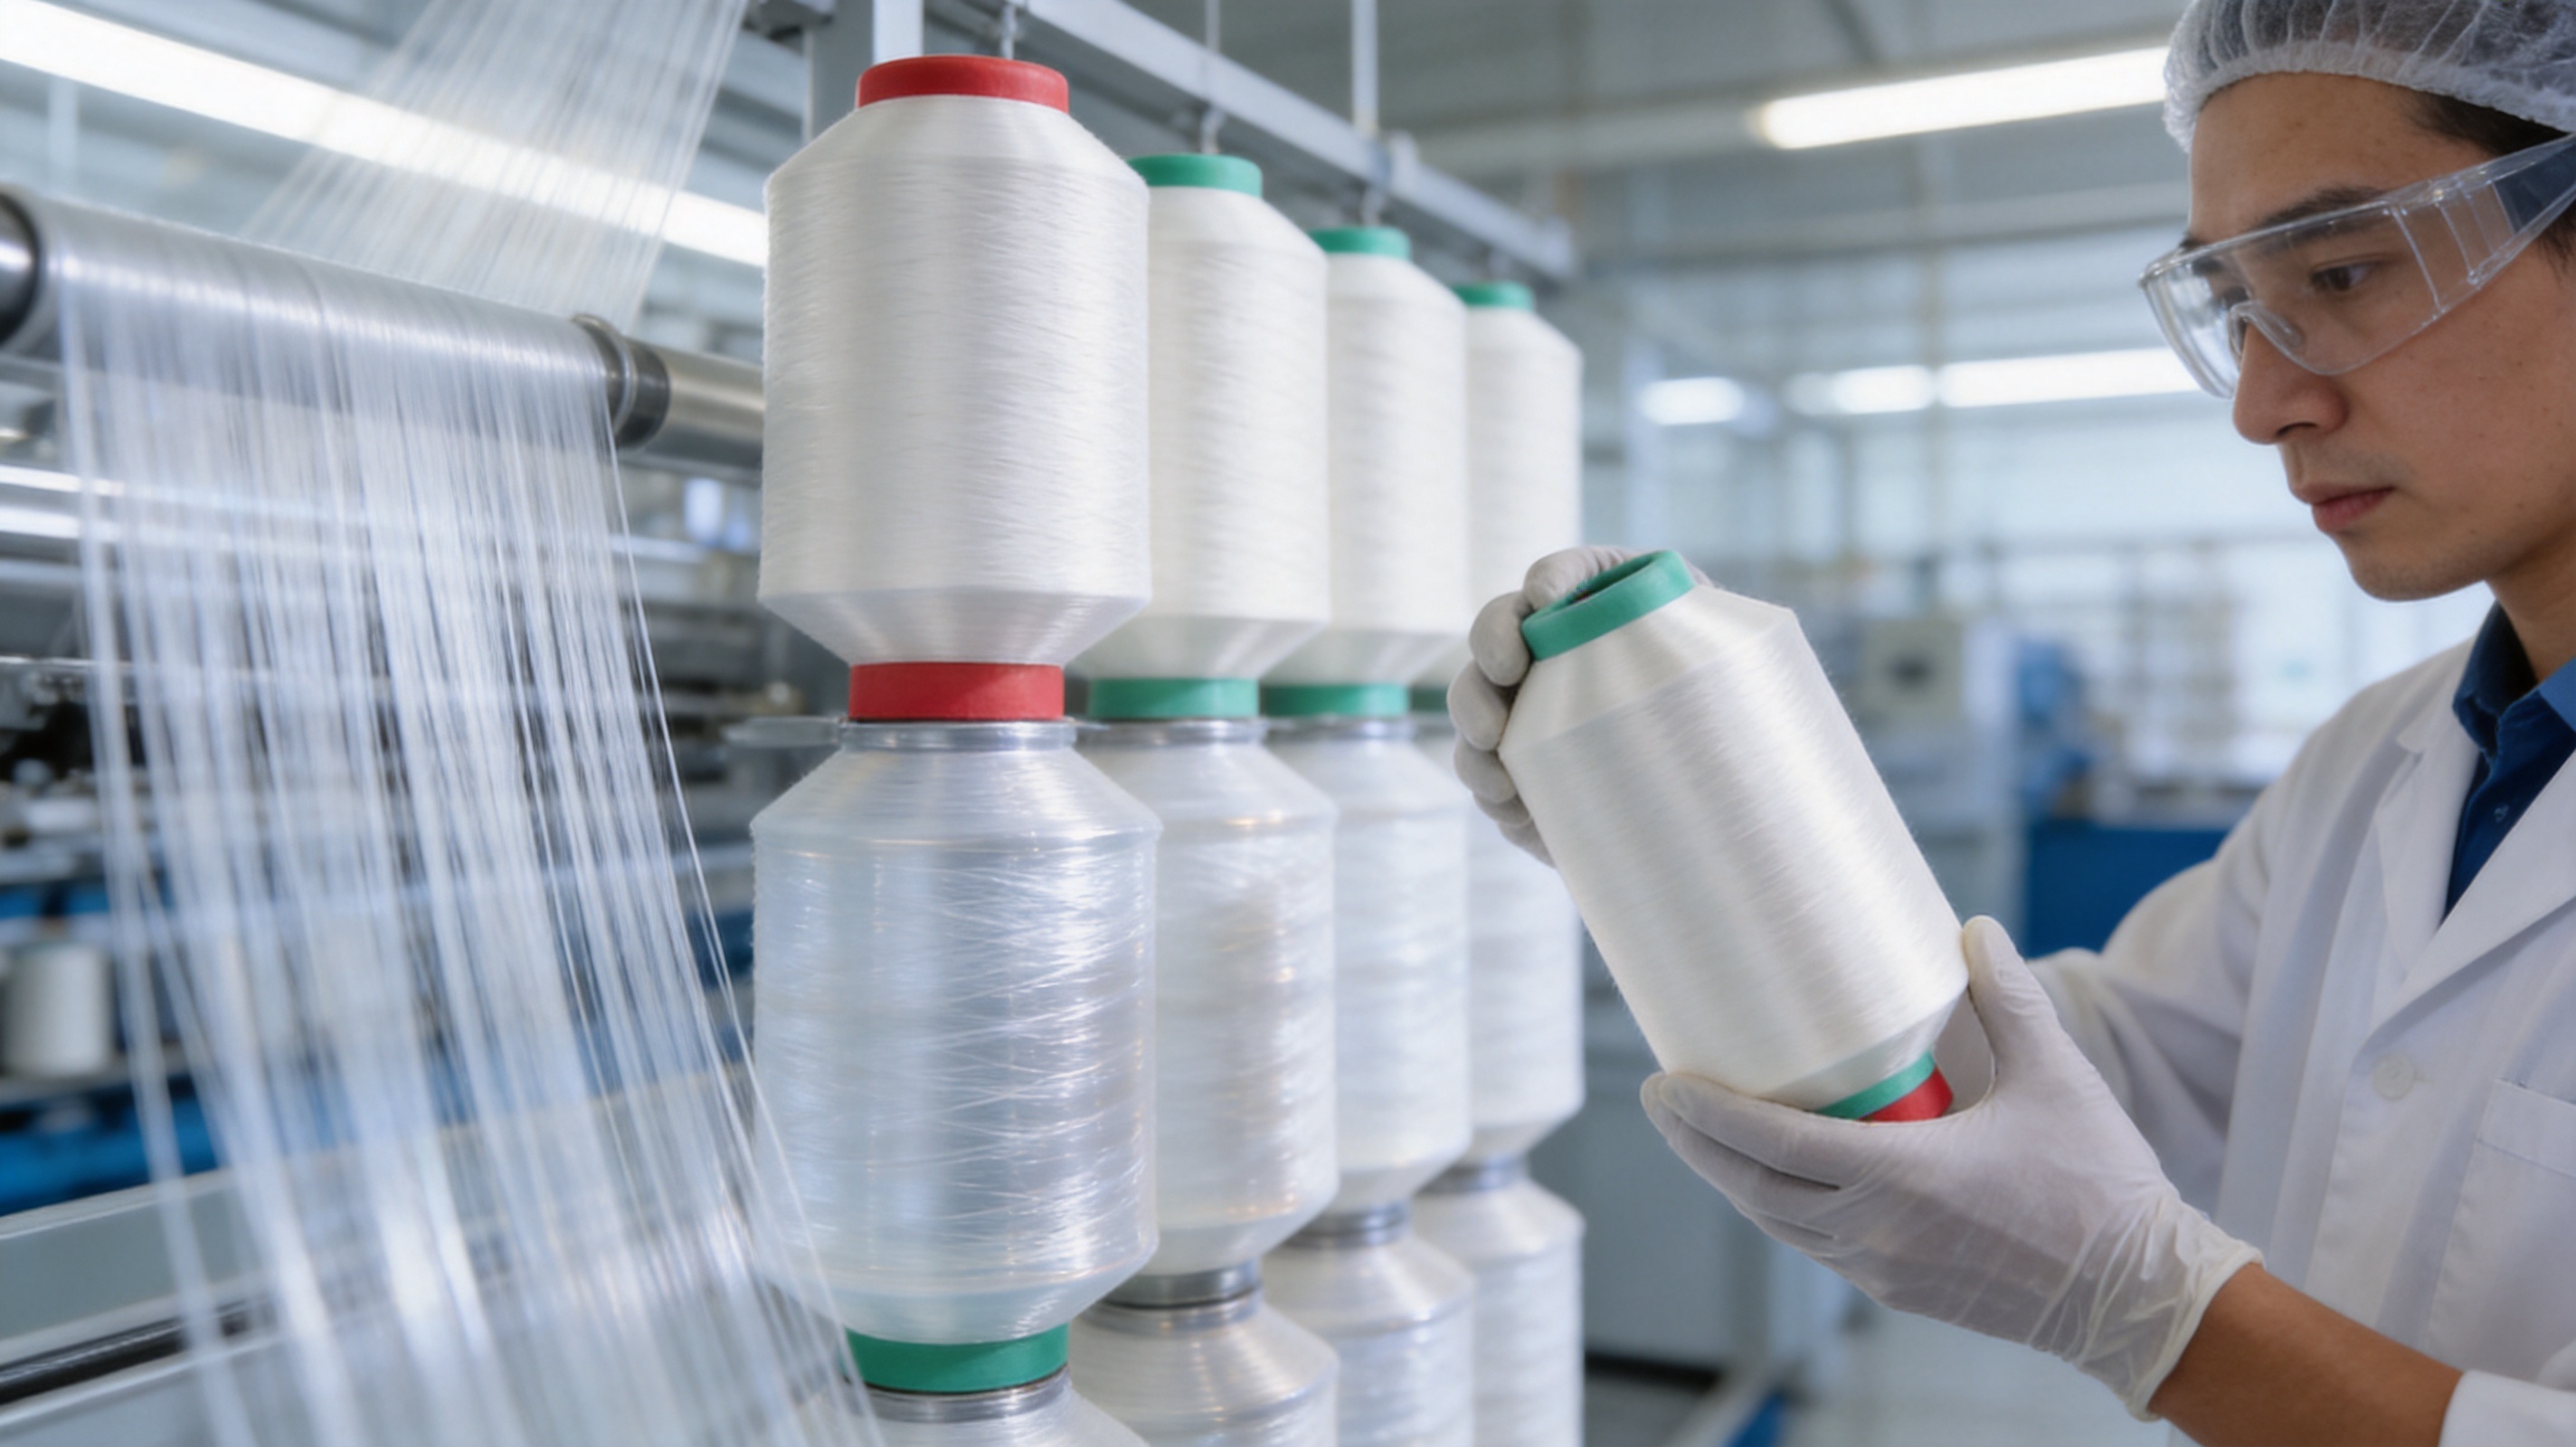
Low melting yarn is not a single universal material category. Different products are based on polyethylene, copolyester, copolyamide, or other polymer systems. Each material has its own temperature range and performance profile. The right choice depends on the finished product and the thermal conditions available in the factory.
| Comparison Point | Pure Nylon Low Melting Yarn | Other Low Melting Yarn Types |
|---|---|---|
| Base polymer | 100% copolyamide nylon | May be PE, copolyester, or another polymer blend |
| Nominal activation point | Approximately 110°C | May range from lower or higher temperature grades |
| Hand feel | Soft and suitable for flexible textile structures | Depends on polymer chemistry and formulation |
| Mechanical behavior | High tenacity and suitable for demanding yarn processing | Varies according to product grade |
| Bonding role | Distributed thermo-fusible bonding agent | May be intended for nonwovens, apparel, industrial, or composite use |
| Typical value | Combines bonding, softness, and textile processability | May prioritize low temperature, stiffness, cost, or high heat resistance |
Lower-temperature polyethylene-based products may activate quickly and can be effective in applications where very low thermal exposure is the main requirement. However, a lower activation temperature is not automatically better. Some applications need a higher degree of mechanical performance, a softer textile hand, or improved compatibility with nylon-based structures.
The 110°C nylon grade provides a balance between moderate activation temperature and high-tenacity textile behavior. It is designed for applications where the bonding component must survive demanding handling before activation and contribute to a flexible, durable structure after activation.
Copolyester low melting yarn is widely used in textile bonding and nonwoven applications. It can offer excellent bonding performance and may be preferred where polyester compatibility or a specific thermal profile is required. However, the final hand feel and mechanical behavior can differ from a pure nylon product.
Pure nylon low melting yarn is an alternative for manufacturers seeking a nylon-based bonding material with a soft touch and high tenacity. It is particularly attractive for nylon-rich textiles, intimate apparel, lace, knitted constructions, and products where flexibility and comfort are central design requirements.
Hot melt powder and film can create strong adhesive layers, but they may require additional coating, scattering, lamination, or positioning operations. Powder distribution can be difficult to control in complex three-dimensional structures, while film can produce a continuous layer that affects drape and breathability.
Low melting yarn distributes the bonding function along a linear textile element. It can be placed exactly where bonding is required or blended into a fiber structure. This approach may offer better control for narrow fabrics, yarn-based composites, knitted forms, and products with irregular geometries.
Liquid adhesives can be useful for many industrial purposes, but they may introduce concerns related to viscosity, coating uniformity, drying time, odor, surface contamination, and equipment cleaning. Low melting yarn is supplied as a solid textile material and can simplify storage and feeding.
It also makes it possible to design bonding into the yarn or fabric architecture rather than applying adhesive only as a surface layer. This can support cleaner edges and help reduce visible adhesive marks, although the final appearance remains dependent on the processing conditions and substrate.
The quality of functional yarn begins with disciplined control of raw materials and continues through polymer preparation, spinning, drawing, thermal treatment, winding, inspection, and packaging. A stable melting point alone is not sufficient. The yarn must also have consistent denier, acceptable tensile performance, reliable surface quality, and predictable processing behavior.
The manufacturing process starts with the selection and preparation of nylon-based raw material appropriate for low melting performance. Polymer quality affects melt viscosity, spinning stability, yarn uniformity, thermal response, and mechanical properties.
Raw materials are managed with attention to cleanliness, moisture, storage conditions, and batch consistency. Nylon is sensitive to moisture, so drying and material handling are important process steps. Proper preparation helps reduce spinning instability and supports more consistent filament formation.
During melt preparation, the polymer is heated in a controlled manner until it reaches the required processing state. Temperature control must be accurate because excessive heat can degrade the polymer, while insufficient heat can create unstable flow or incomplete melting.
Modern production systems use monitored heating zones, controlled residence time, and filtration systems to help maintain clean and stable polymer flow. The objective is to produce a uniform melt that can be extruded into filaments with consistent diameter and surface quality.
In the spinning stage, the prepared polymer passes through a spinneret to form continuous filaments. Spinneret design, hole geometry, throughput, cooling conditions, and take-up speed all influence the final yarn structure.
Stable spinning is especially important for fine counts such as 20D, 30D, and 40D. These specifications require accurate control because small changes in filament diameter can affect strength, appearance, winding behavior, and bonding distribution. Heavier counts such as 150D, 200D, or 300D also require carefully managed throughput and cooling to maintain uniformity.
After extrusion, the filaments are cooled and solidified. Cooling must be sufficiently uniform to prevent differences in crystallization, orientation, and surface structure across the yarn bundle.
Uneven cooling can contribute to variations in shrinkage, elongation, strength, and thermal response. Controlled airflow and stable production conditions therefore play an important role in producing yarn that behaves consistently during later processing.
Drawing aligns the molecular structure of the filament and improves mechanical performance. The drawing ratio, roller temperature, speed relationship, and tension profile must be selected according to the intended yarn grade.
For low melting yarn, drawing requires a careful balance. Excessive orientation may affect the desired thermal response, while insufficient orientation may reduce tenacity and create unstable processing. The manufacturing objective is to produce yarn that is strong enough for high-speed handling while retaining its designed melting characteristics.
Thermal treatment can be used to control dimensional stability, shrinkage behavior, and yarn performance. The treatment must be designed so that the yarn remains stable in normal processing but still activates appropriately when exposed to the intended bonding temperature.
Process engineers evaluate the relationship between heat treatment, yarn tension, elongation, shrinkage, and melting behavior. This is one of the reasons that specialized production experience is important for functional yarns: a small process change can influence both mechanical and thermal performance.
After spinning and treatment, the yarn is wound onto paper tubes, wax tubes, or other suitable packages. Package density and winding tension are controlled to support smooth storage, transport, unwinding, and downstream processing.
A well-formed package should feed consistently without excessive friction or sudden tension changes. This is essential for automatic sewing, computerized knitting, braiding, rewinding, and other high-speed operations. Packaging can be customized according to machine requirements and order specifications.
Quality control can include visual inspection, denier testing, tensile testing, elongation testing, melting-point evaluation, package inspection, and process documentation. Depending on the application, additional checks may be conducted for shrinkage, bonding behavior, color, moisture, and surface consistency.
Actual values should be confirmed through the technical documents and test reports associated with each batch. Reference specifications are useful for product selection, but production orders should be controlled according to agreed technical requirements and application trials.
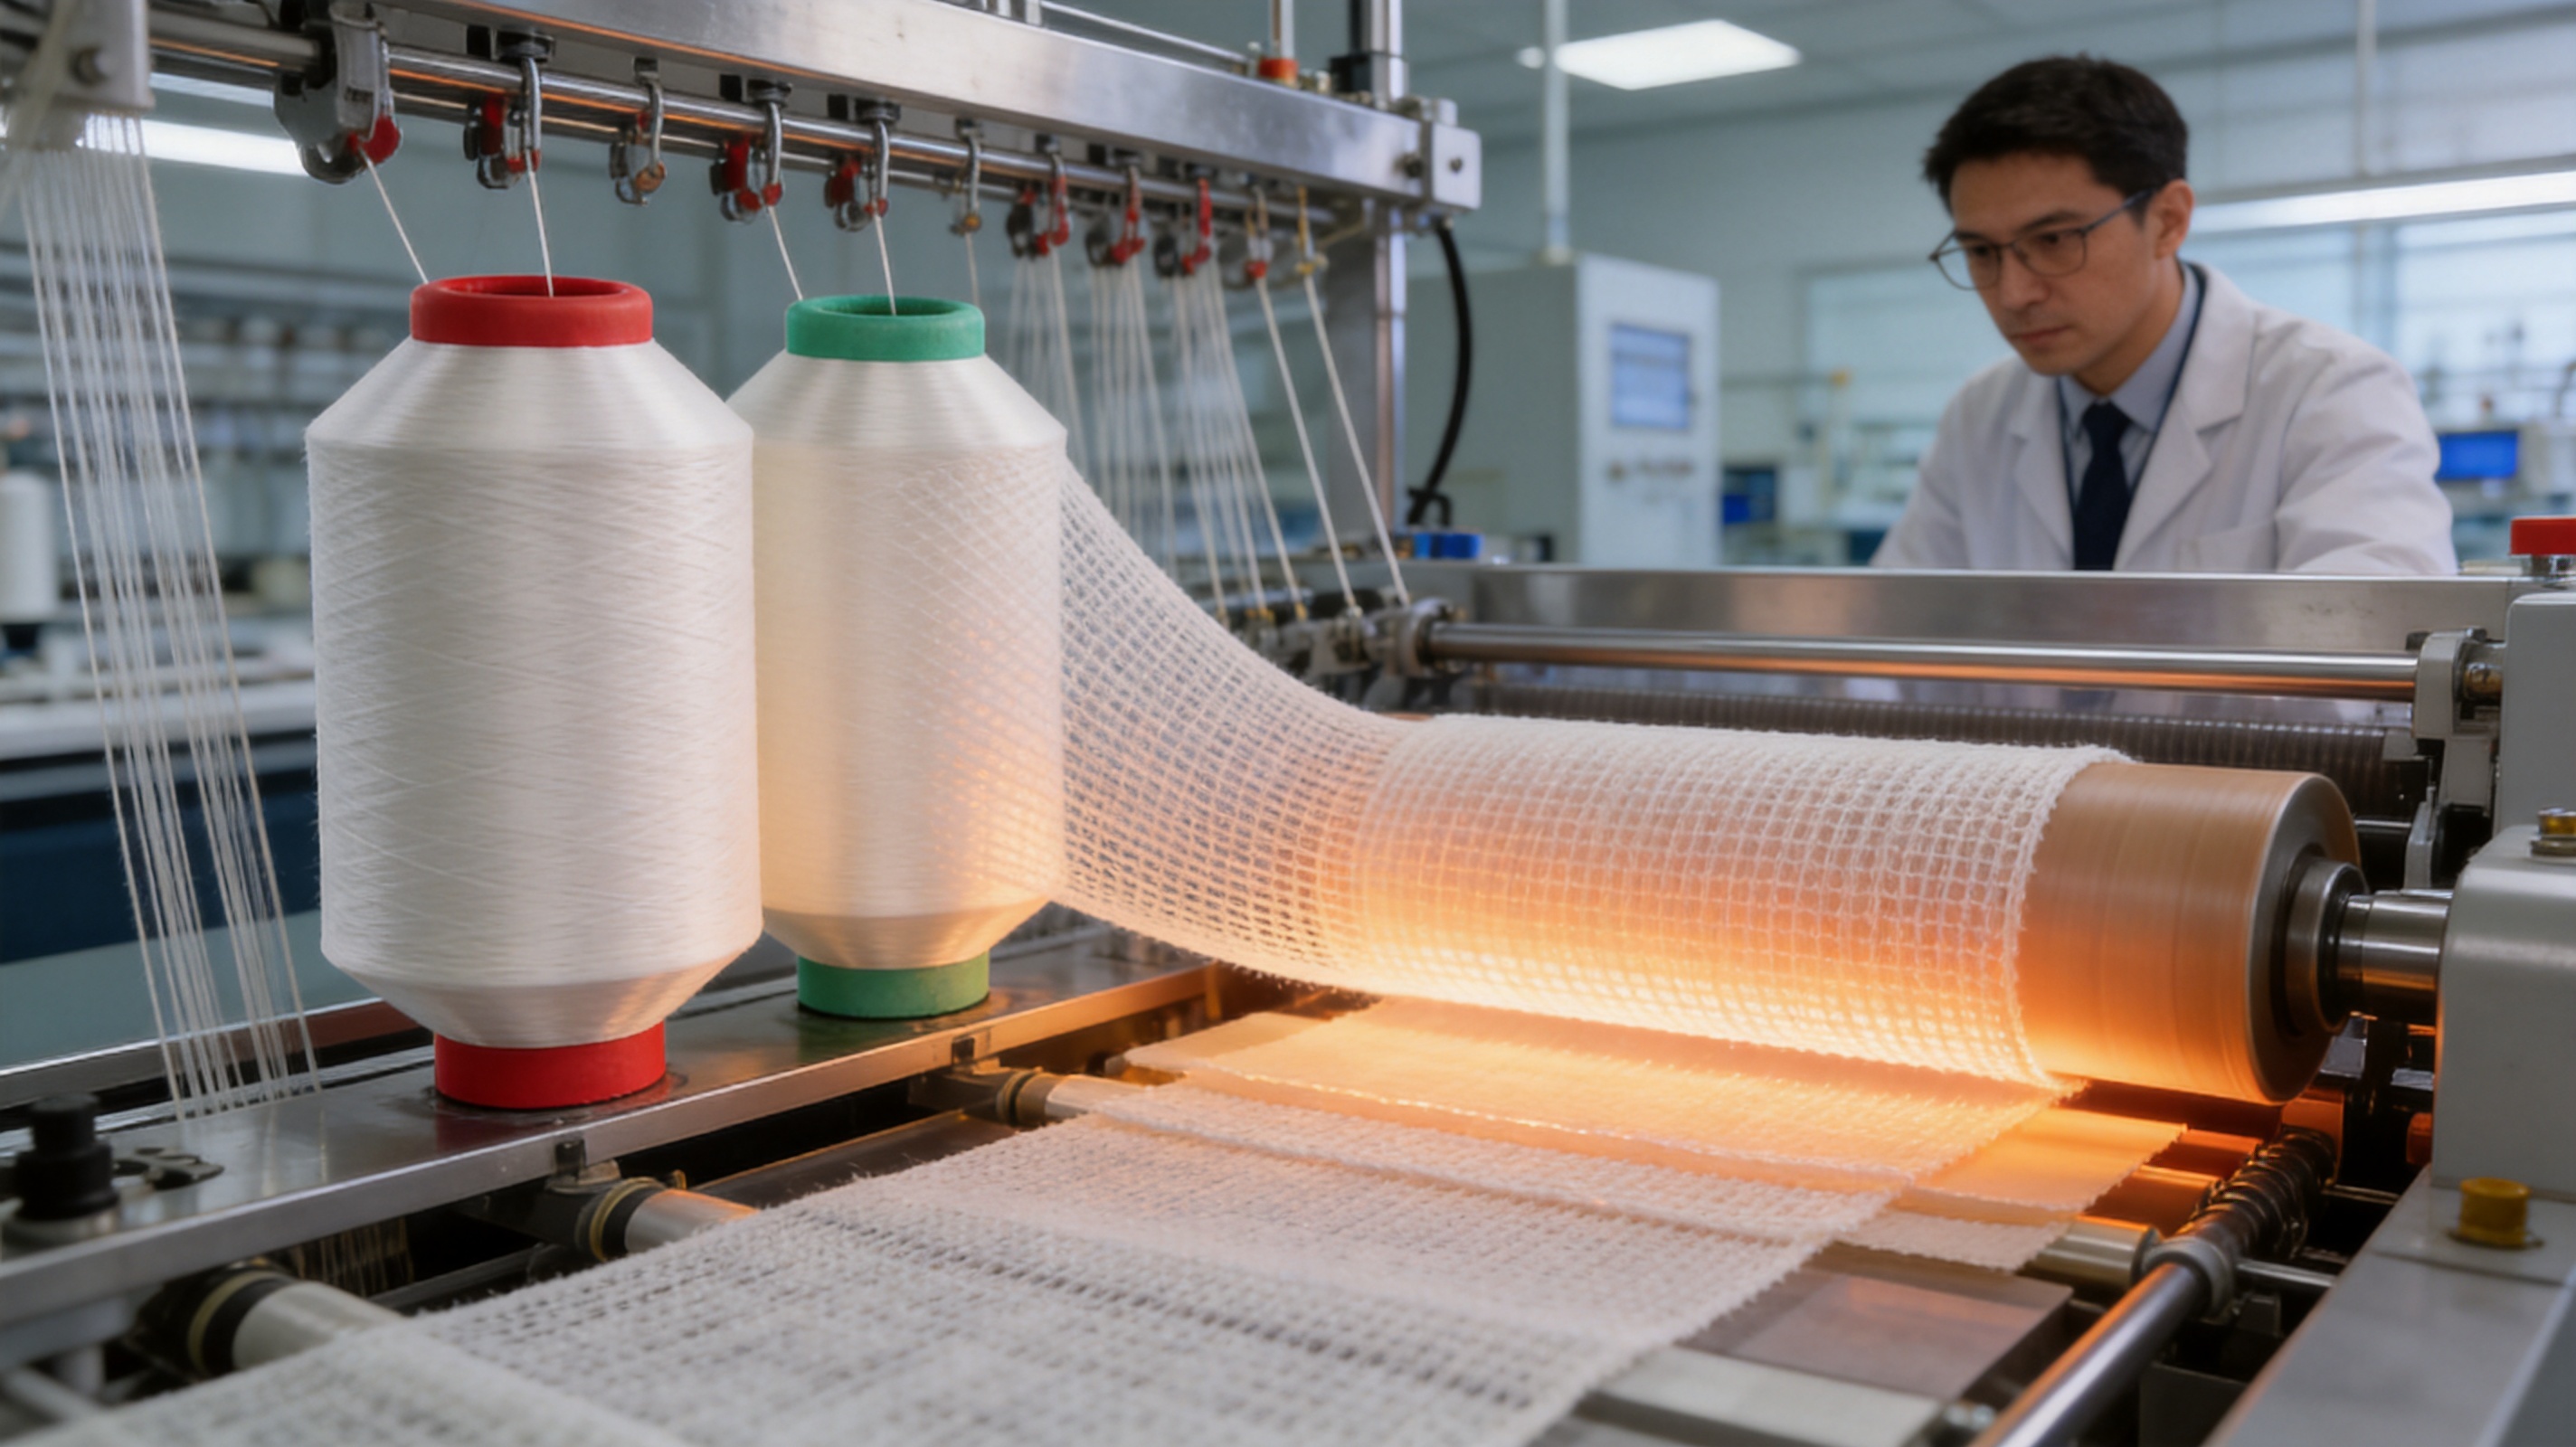
A specialized functional yarn manufacturer contributes more than a single catalog specification. Product consistency, application knowledge, customization ability, production flexibility, and communication between sales, research, development, design, and manufacturing teams all affect the success of a customer project.
The manufacturer described in the supplied materials has operated as a special textile factory in China since 2006. Its product portfolio includes biodegradable yarn, low melting yarn, ECDP yarn, anti-static yarn, HDPE yarn, bio-component yarn, and polyester filament yarn.
This broad portfolio is valuable because customers often need to compare several functional materials before selecting the most suitable solution. A manufacturer familiar with different polymer systems can provide more useful guidance on melting point, hand feel, tenacity, sustainability objectives, and compatibility with downstream processes.
Functional yarn development requires more than standard spinning knowledge. It involves understanding polymer behavior, filament formation, thermal activation, textile construction, and end-use requirements. A dedicated design and research team can help adapt yarn parameters to a particular machine or product.
Customization may include denier, filament count, cross-sectional structure, color, packing format, winding specification, and selected functional properties. The exact scope depends on equipment capability, order volume, raw materials, and technical feasibility.
Some customers need a product that is not available as a standard item. For example, a shoe manufacturer may require a specific melting behavior in a three-dimensional knitted upper, while a narrow-fabric producer may need a fine yarn with a particular package size and bonding response.
Collaborative development allows the manufacturer and customer to define the target application, identify the relevant performance indicators, prepare samples, evaluate processing conditions, and refine the specification. This approach helps prevent the common problem of choosing a yarn based only on denier or melting point without considering the complete production system.
Multiple production lines and machines can help accommodate both customized orders and larger-volume requirements. Production flexibility is particularly important for functional yarn because customers may begin with small sample quantities before moving to regular production.
Strong control over raw material supply and manufacturing conditions can also support more stable repeat orders. For industrial users, continuity between sample, pilot, and mass production is a major purchasing consideration.
Technical support should continue beyond the quotation stage. Customers may need help with yarn selection, machine compatibility, package design, testing conditions, sample evaluation, and production troubleshooting.
A professional team can help clarify whether the application requires a fine or heavy denier, a specific filament arrangement, a particular package, or a different low melting grade. It can also help distinguish between a problem caused by the yarn and one caused by temperature, pressure, dwell time, fabric composition, or machine setup.
The listed count options include 20D, 30D, 40D, 50D, 70D, 100D, 150D, 200D, and 300D. The appropriate selection depends on the required bonding quantity, textile construction, machine feeding system, target softness, and final strength.
| Approximate Count Group | Potential Product Direction | Selection Considerations |
|---|---|---|
| 20D–40D | Fine lace, lingerie ribbon, delicate knitted structures, fine bonding details | Prioritize low visual impact, flexibility, and controlled feeding |
| 50D–100D | Apparel, seamless underwear, narrow fabrics, moderate bonding applications | Balance softness, coverage, tenacity, and bonding distribution |
| 150D–200D | Three-dimensional knitted structures, chenille systems, ropes, technical textiles | Consider mechanical load, construction thickness, and equipment compatibility |
| 300D | Heavy-duty or industrial textile structures | Evaluate required bonding quantity, processing tension, and final composite strength |
The count alone does not determine performance. Filament count, yarn structure, twist or wrapping method, package form, blend percentage, and processing temperature can all change the final result. Customers should provide information about the machine, base fabric, target use, required hand feel, and expected production volume when requesting a recommendation.
Three-dimensional knitted structures often require localized stabilization without losing flexibility. Low melting yarn can be incorporated into selected zones and activated after knitting, helping hold the structure in place.
This is relevant to footwear uppers, sports equipment, protective padding, molded textile components, and other products where shape retention and breathability must be balanced. The yarn can contribute to structural support while maintaining a softer textile surface than some rigid reinforcement materials.
In knitted shoe uppers, the bonding yarn can help stabilize areas that experience repeated flexing, tension, or deformation. It may be used with flyknit-style constructions, sports gloves, activewear accessories, and other performance products.
Successful use depends on the complete upper design. The processor must consider the base yarn, knitting density, activation method, pressure, cooling conditions, and the areas where support is required. Sample trials are essential because too much bonding can reduce flexibility, while too little may not provide sufficient structural support.
Low melting yarn can function as a bonding or core component in chenille yarn systems. It may help hold surrounding fibers or pile elements in position after thermal activation.
The correct yarn count and processing conditions depend on the chenille construction, pile density, core material, wrapping method, and desired softness. The bonding effect should be strong enough to improve stability without damaging the visual fullness or tactile character of the chenille yarn.
Fine counts can be suitable for delicate ribbons, lace, narrow fabrics, and decorative textile components. These products often require clean edges, soft touch, and resistance to fraying without creating a visible rigid line.
Thermal bonding can help secure edge structures, join layers, or stabilize selected decorative patterns. The moderate activation temperature may be useful where the base material is sensitive to high heat, but trials are necessary to confirm color stability, dimensional behavior, and final comfort.
Bonded sewing thread requires a controlled surface and reliable mechanical behavior. A thermo-fusible nylon yarn can support bonding between thread components or help stabilize a sewn structure when activated under appropriate conditions.
It may be considered for industrial sewing, technical textile assembly, protective products, and applications where reduced fraying or improved thread integrity is required. The sewing machine needle, tension, stitch density, and thermal activation conditions should be evaluated together.
Seamless underwear combines comfort, elasticity, close contact with the skin, and dimensional stability. Low melting yarn can be used to reinforce selected areas or help create bonded structures without adding bulky seams.
The soft hand feel of pure nylon is a significant advantage in this application. However, the finished garment must be tested for stretch recovery, wash durability, skin comfort, and resistance to peeling after repeated laundering.
In ropes, cords, and narrow technical structures, low melting yarn can help stabilize the relationship between component fibers. It may be used as a bonding thread, core element, or wrapping material.
The final performance depends on the rope architecture, load direction, elongation requirements, thermal process, and environmental exposure. For heavy-duty applications, bonding yarn should complement rather than replace the main load-bearing fibers unless the complete structure has been specifically engineered for that purpose.
Thermo-fusible yarn can be incorporated into protective textile layers around cables or wires. When activated, it may help hold the textile covering in position and reduce movement between components.
This can support cleaner construction and improved shape retention in protective sleeves, cable wraps, and composite sheathing. Electrical, thermal, flame, abrasion, and regulatory requirements must be considered separately according to the intended cable application.
Low melting yarn or fiber can serve as a bonding component in thermal-bonded nonwovens, pillow filling, quilt filling, mattress structures, sofa composites, and other textile cores. It can help create a bonded network without relying entirely on sprayed adhesive.
The blend ratio and heating system are especially important in these applications. The material must reach sufficient activation throughout the thickness of the nonwoven without causing unacceptable shrinkage, hard spots, odor, or loss of loft.
In apparel interlining, the bonding yarn can provide structure and support while maintaining a relatively flexible hand. It may be incorporated into the interlining or used as part of a fusible textile system.
Press temperature, pressure, dwell time, and cooling should be controlled carefully. The finished garment should be evaluated after washing, dry cleaning if applicable, stretching, and repeated use.
Automotive interior insulation composites may use thermal bonding to hold fibrous layers together. A nylon-based low melting material can be considered where a flexible composite, controlled bonding temperature, and stable fiber network are required.
Automotive applications involve demanding requirements for temperature resistance, odor, aging, flammability, vibration, and dimensional stability. The yarn must be assessed within the entire composite system and against the applicable customer or industry standards.
The bonding process can be understood as a sequence of preparation, heating, flow, penetration, cooling, and solidification.
The final bond is influenced by several variables. Temperature must be high enough to activate the yarn but not so high that it damages the base material. Dwell time must allow sufficient heat transfer through the structure. Pressure can improve contact, but excessive pressure may flatten the textile or reduce loft. The blend ratio determines how much bonding material is available, while cooling conditions influence the final shape and stress distribution.
Before mass production, a trial should be performed using the actual base material and production equipment. Laboratory heating data cannot always predict factory results because heat transfer differs between a thin lace, a thick knitted upper, a rope, and a multilayer nonwoven.
The trial should evaluate yarn feeding, machine tension, thermal activation, appearance, bonding strength, flexibility, dimensional stability, and post-treatment behavior. If the application involves garments, testing should include repeated washing and drying. If the application involves technical composites, testing should include mechanical loading, aging, abrasion, and environmental exposure as appropriate.
Storage conditions should also be controlled. Yarn packages should be protected from excessive moisture, contamination, direct sunlight, and extreme temperature. Proper storage helps preserve unwinding behavior and supports consistent processing.
When changing from one yarn count to another, the customer should review feeding tension, package size, blend ratio, machine settings, and activation conditions. A heavier count may deliver more bonding polymer but may also require different guides, needle settings, or thermal exposure.
Low melting yarn can support a more efficient and cleaner bonding process in applications where it replaces or reduces liquid adhesive. It is a solid textile material that can be measured, fed, positioned, and stored without the same handling requirements associated with many wet adhesive systems.
Reducing adhesive application may also help reduce surface contamination, drying operations, solvent exposure, and workplace odor. The environmental benefit depends on the complete product life cycle, including polymer sourcing, production energy, transport, processing temperature, durability, and end-of-life treatment.
The product should therefore be described as a potential eco-conscious bonding alternative rather than automatically classified as biodegradable. Pure nylon is not the same as biodegradable yarn. Its sustainability value comes primarily from possible process simplification, reduced adhesive use, durable performance, and the ability to create lighter or more efficient textile structures where appropriate.
Durability can also contribute to resource efficiency. If thermal bonding helps prevent fraying, peeling, or structural deformation, the finished article may maintain its function for longer. However, durability claims must be verified for each application through standardized testing.
Customized production is important when a standard yarn does not fully meet a customer’s technical needs. An OEM or development project may involve a custom denier, filament count, cross-section, package, color, melting range, tenacity level, or surface characteristic.
Denier affects the amount of polymer delivered, visual presence, flexibility, and mechanical behavior. Filament count affects yarn compactness, surface feel, splitting behavior, and processing characteristics. These parameters can be adjusted within the manufacturer’s technical capabilities.
Special cross-sections may be considered when a customer needs a specific surface area, friction behavior, luster, or bonding distribution. The feasibility of a customized cross-section depends on spinneret design, polymer behavior, production volume, and quality requirements.
Packages can be adapted to downstream machinery. Paper tubes, wax tubes, and other formats may be considered according to unwinding speed, machine clearance, package weight, and customer handling preferences.
The most effective customization begins with the application rather than with a single specification. The customer should provide the base material, machine type, production speed, thermal equipment, target bond strength, desired hand feel, washing or aging requirements, and expected order quantity.
The manufacturer can then evaluate whether the 110°C pure nylon grade is appropriate or whether another low melting temperature or polymer system should be considered. Sample testing and technical communication help reduce the risk of selecting a material that performs well in theory but does not run efficiently on the customer’s equipment.
It is a thermo-fusible yarn made from a pure nylon or copolyamide polymer system. At approximately 110°C, it softens or melts and can bond nearby fibers or textile components. After cooling, it forms bonding points that help stabilize the structure.
110°C is the nominal design point or reference melting range. The actual production setting should be established through trials because equipment type, fabric thickness, pressure, dwell time, line speed, and machine calibration all affect the required temperature.
It can reduce or replace liquid adhesive in selected applications. The extent of replacement depends on the required bond strength, wash resistance, flexibility, substrate, processing conditions, and cost target. A production trial is necessary before making a complete substitution.
Pure nylon low melting yarn uses a different polymer system and is designed to combine a soft hand feel with high tenacity and moderate thermal activation. PE products may offer lower-temperature bonding or different chemical and mechanical behavior. The best choice depends on the application.
Copolyester grades are often selected for polyester-compatible systems and specific bonding requirements. Pure nylon is an alternative for customers seeking nylon-based performance, soft touch, high tenacity, and compatibility with flexible nylon-rich textile structures.
The listed options include 20D, 30D, 40D, 50D, 70D, 100D, 150D, 200D, and 300D. The final available specification should be confirmed according to the production order, application, and technical requirements.
Yes, fine counts may be suitable for lace, lingerie ribbons, seamless underwear, and narrow fabrics. The processing conditions must be carefully controlled to preserve softness, appearance, elasticity, and comfort.
It can be considered as a bonding or stabilizing component in ropes and cords. The yarn should not be assumed to replace the primary load-bearing material. Final rope performance must be tested according to the intended load, construction, and environment.
Yes. It may help stabilize selected areas of three-dimensional knitted uppers and sports textile structures. The knitting design, yarn placement, thermal activation, pressure, and cooling conditions should be optimized through trials.
Pure nylon low melting yarn should not be described as biodegradable unless a specific certified biodegradable formulation is supplied. It is a functional nylon bonding yarn. Its potential sustainability benefits relate to process efficiency, reduced adhesive use, durability, and material optimization.
Possible systems include hot air, steam, heat presses, heated rollers, calendering equipment, and industrial ovens. The appropriate system depends on the product geometry, thickness, production speed, and desired bonding pattern.
Selection should consider the amount of bonding required, the base textile, machine feeding system, visual impact, flexibility, final strength, and production speed. Fine counts are commonly considered for delicate products, while heavier counts may be suitable for thicker or more technical structures.
Customized development may include denier, filament count, cross-section, color, package format, and selected functional properties. Feasibility depends on technical requirements, available equipment, raw materials, order volume, and development conditions.
Useful information includes the intended application, base material, yarn count, machine type, production speed, required package, target melting behavior, bond strength, color, estimated quantity, testing requirements, and delivery expectations.
The supplied product information identifies Shanghai seaport as the shipping port. Final logistics arrangements should be confirmed with the manufacturer according to order terms, destination, packaging, and shipping schedule.
A structured evaluation helps determine whether 110°C pure nylon low melting yarn is suitable for a particular production line. The first step is to confirm the polymer and thermal requirement. If the base material cannot tolerate the activation temperature, another grade or another bonding method may be needed.
The second step is to evaluate mechanical handling. The yarn should run through the customer’s actual guides, needles, tensioners, sewing heads, or winding equipment. Smooth feeding and low breakage are important indicators of process compatibility.
The third step is to assess the bonded structure. Testing should include peel strength where relevant, tensile strength, flexing, elongation, dimensional stability, visual appearance, hand feel, and resistance to fraying or delamination.
The fourth step is to conduct end-use testing. Garments may require washing, drying, stretching, and skin-contact assessment. Footwear may require flexing, abrasion, moisture, and bonding durability tests. Industrial composites may require heat aging, vibration, compression, tensile loading, and environmental exposure tests.
The final step is to confirm production consistency. A supplier should be able to communicate the reference specification, packing method, quality-control approach, customization options, and batch documentation. Consistent supply is essential when the yarn becomes part of a repeat industrial process.
Pure Nylon Low Melting Yarn at approximately 110°C is a versatile bonding material for textile manufacturers seeking a combination of thermal functionality, softness, high tenacity, and smooth processing. Its 100% copolyamide construction differentiates it from PE and copolyester alternatives and makes it especially relevant to nylon-rich, flexible, delicate, and three-dimensional textile structures.
The yarn can serve as a distributed solid-state adhesive in three-dimensional knitted fabric, footwear uppers, chenille yarn, lingerie ribbon, lace, bonded sewing thread, seamless underwear, ropes, cable wire protection, nonwovens, interlinings, insulation composites, and home textile filling.
Its main technical advantages include a controlled 110°C activation point, soft hand feel, high tenacity, easy rewinding, stable processing behavior, flexible bonding, and the potential to reduce dependence on liquid adhesives. The strongest results are achieved when the yarn count, blend ratio, package, machine settings, heating method, and cooling conditions are selected for the complete application rather than judged independently.
Advanced polymer preparation, precision spinning, controlled drawing, thermal stabilization, accurate winding, and systematic quality inspection are essential to producing a reliable functional yarn. Equally important are research and development capability, customization support, production flexibility, and close cooperation with customers during sampling and scale-up.
For buyers evaluating this product, the most practical approach is to begin with a representative sample, test it on the actual equipment, and measure both processing behavior and finished-product performance. When the material is correctly matched to the application, 110°C pure nylon low melting yarn can provide a clean, efficient, and technically effective route to textile bonding and structural stabilization.
1. General principles of polymer melt processing and thermoplastic fiber spinning.
2. Textile fiber testing practices for denier, tenacity, elongation, shrinkage, and package quality.
3. Technical guidance on thermal bonding of nonwoven fabrics and fiber-based composites.
4. Industrial practices for hot melt bonding, heat pressing, calendering, and thermal lamination.
5. General performance considerations for polyamide fibers in apparel, technical textiles, and composite structures.
6. Manufacturer-supplied product information for pure nylon low melting yarn with an approximately 110°C melting point.
7. Manufacturer-supplied information concerning functional yarn development, customized production, packaging, and application support.
Made of PBS (Polybutylene Succinate), fully biodegradable.Features:1.Home compostable2.Raw material: PBS Polybutylene Su...
READ MOREPlease fill out the form below and our team will contact you as soon as possible.
Addres: No.66 Qiaogang Road, Haian, Nantong City, Jiangsu Province, China
E-mail: service@gcfiber.com admin@gcfiber.com
Copyright ? GC FIBER All Rights Reserved. Eco-Friendly Textile Products Manufacturer Biodegradable Yarn Company